 English
Engineering Purity & Active Potency from Source to Standardized Extract
Headquartered in the botanical extraction heartland of Xi'an, Shaanxi, BKYULA Biotech Co., Ltd. is a dedicated manufacturer and global exporter of high-potency plant extracts, functional feed additives, fruit and vegetable powders, and dietary supplement ingredients. With an established operation supported by 67 full-time personnel, 4 dedicated R&D formulation scientists, and 3 certified QA/QC analytical inspectors, we maintain end-to-end control from raw botanicals to packaged bulk powders.
Our facilities have undergone rigorous on-site verification by SGS Group, assessing legal operational legitimacy, machinery scale, quality assurance workflows, and traceability. Combining advanced multi-stage extraction, low-temperature vacuum concentration, and precise spray drying, BKYULA Biotech serves procurement teams across North America, Latin America, Europe, and Asia with uncompromising batch consistency.
Verified buyer satisfaction index stands 4.1% higher than regional industry benchmarks across product authenticity, lead-time precision, and compliance documentation.
End-to-End Botanical Extraction Process
From botanical raw materials through multi-stage refining to clean-room packaging, our six core stages safeguard phytochemical potency and microbiological sterility.
 Step 01
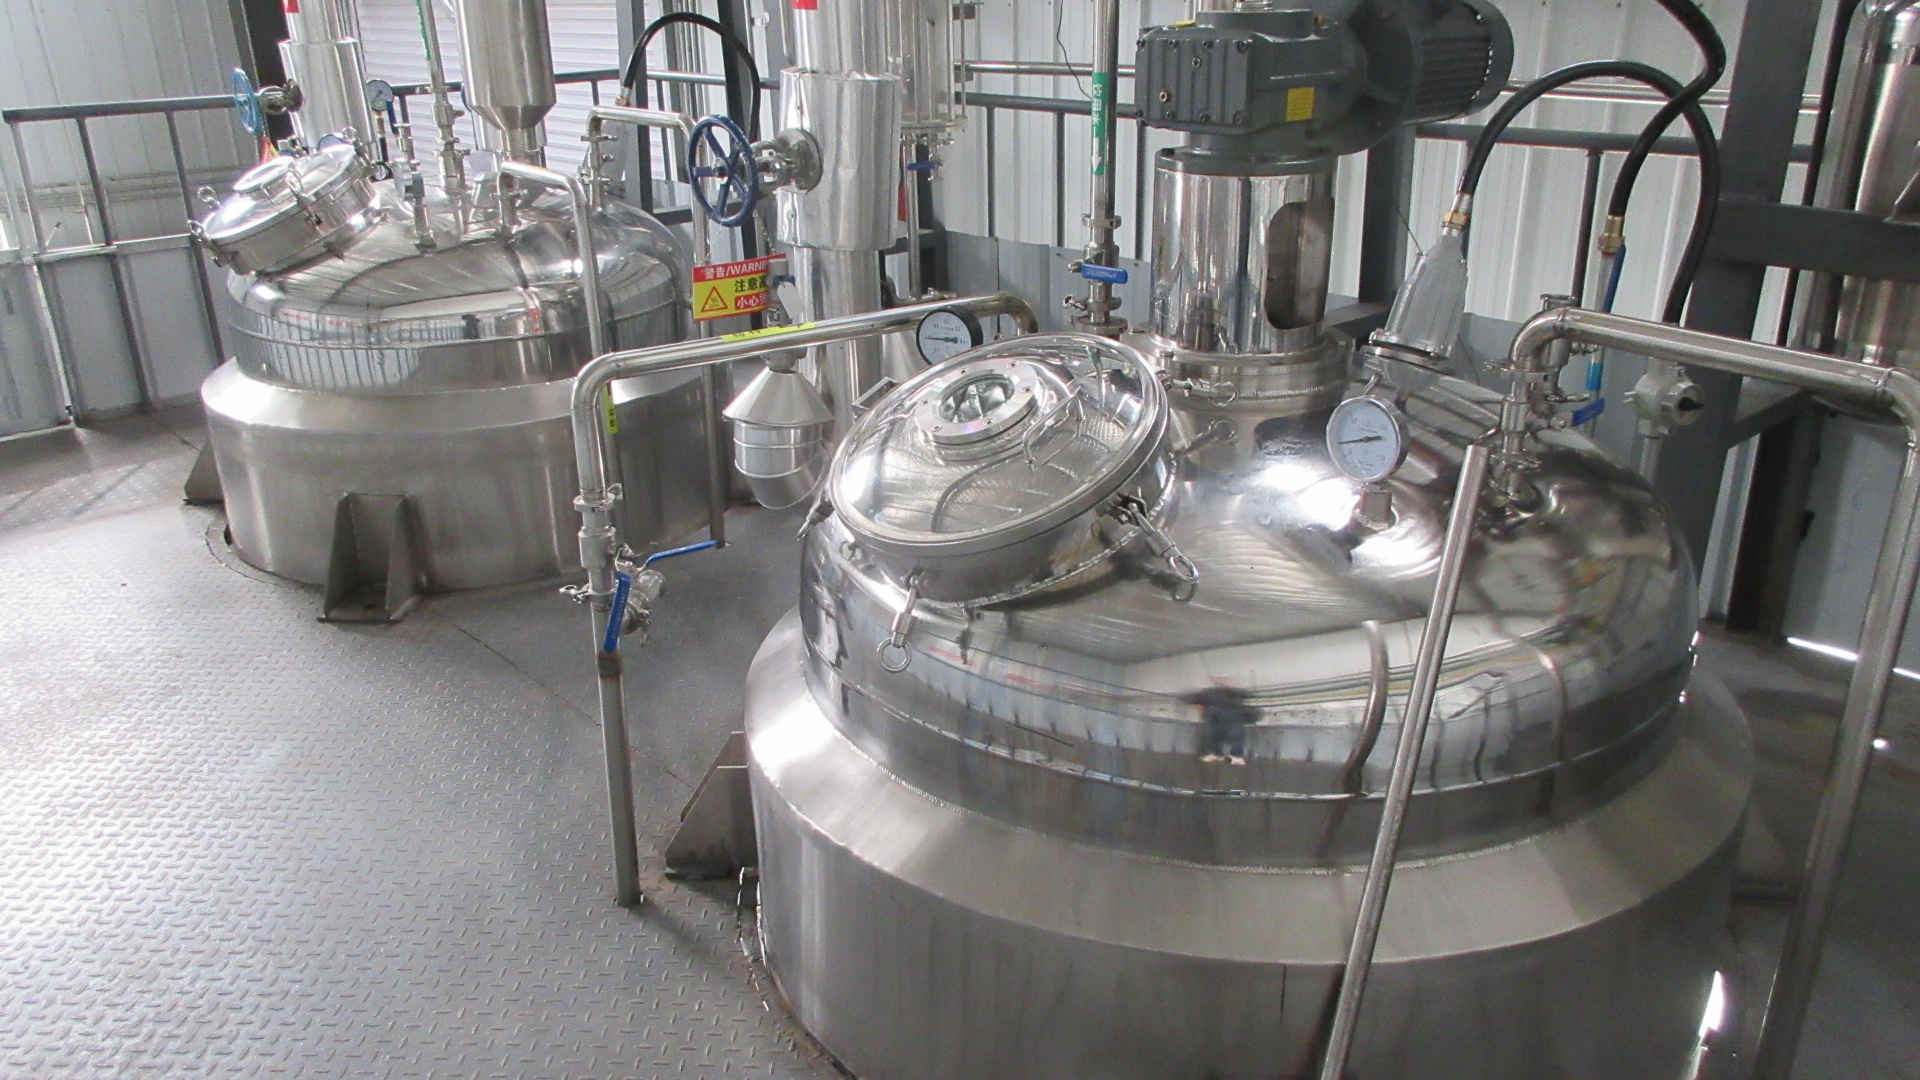
Standardized Extraction
Aqueous or multi-ratio ethanol solvent extraction in multi-functional 316 stainless-steel vessels under automated temperature and duration controllers.
 Step 02
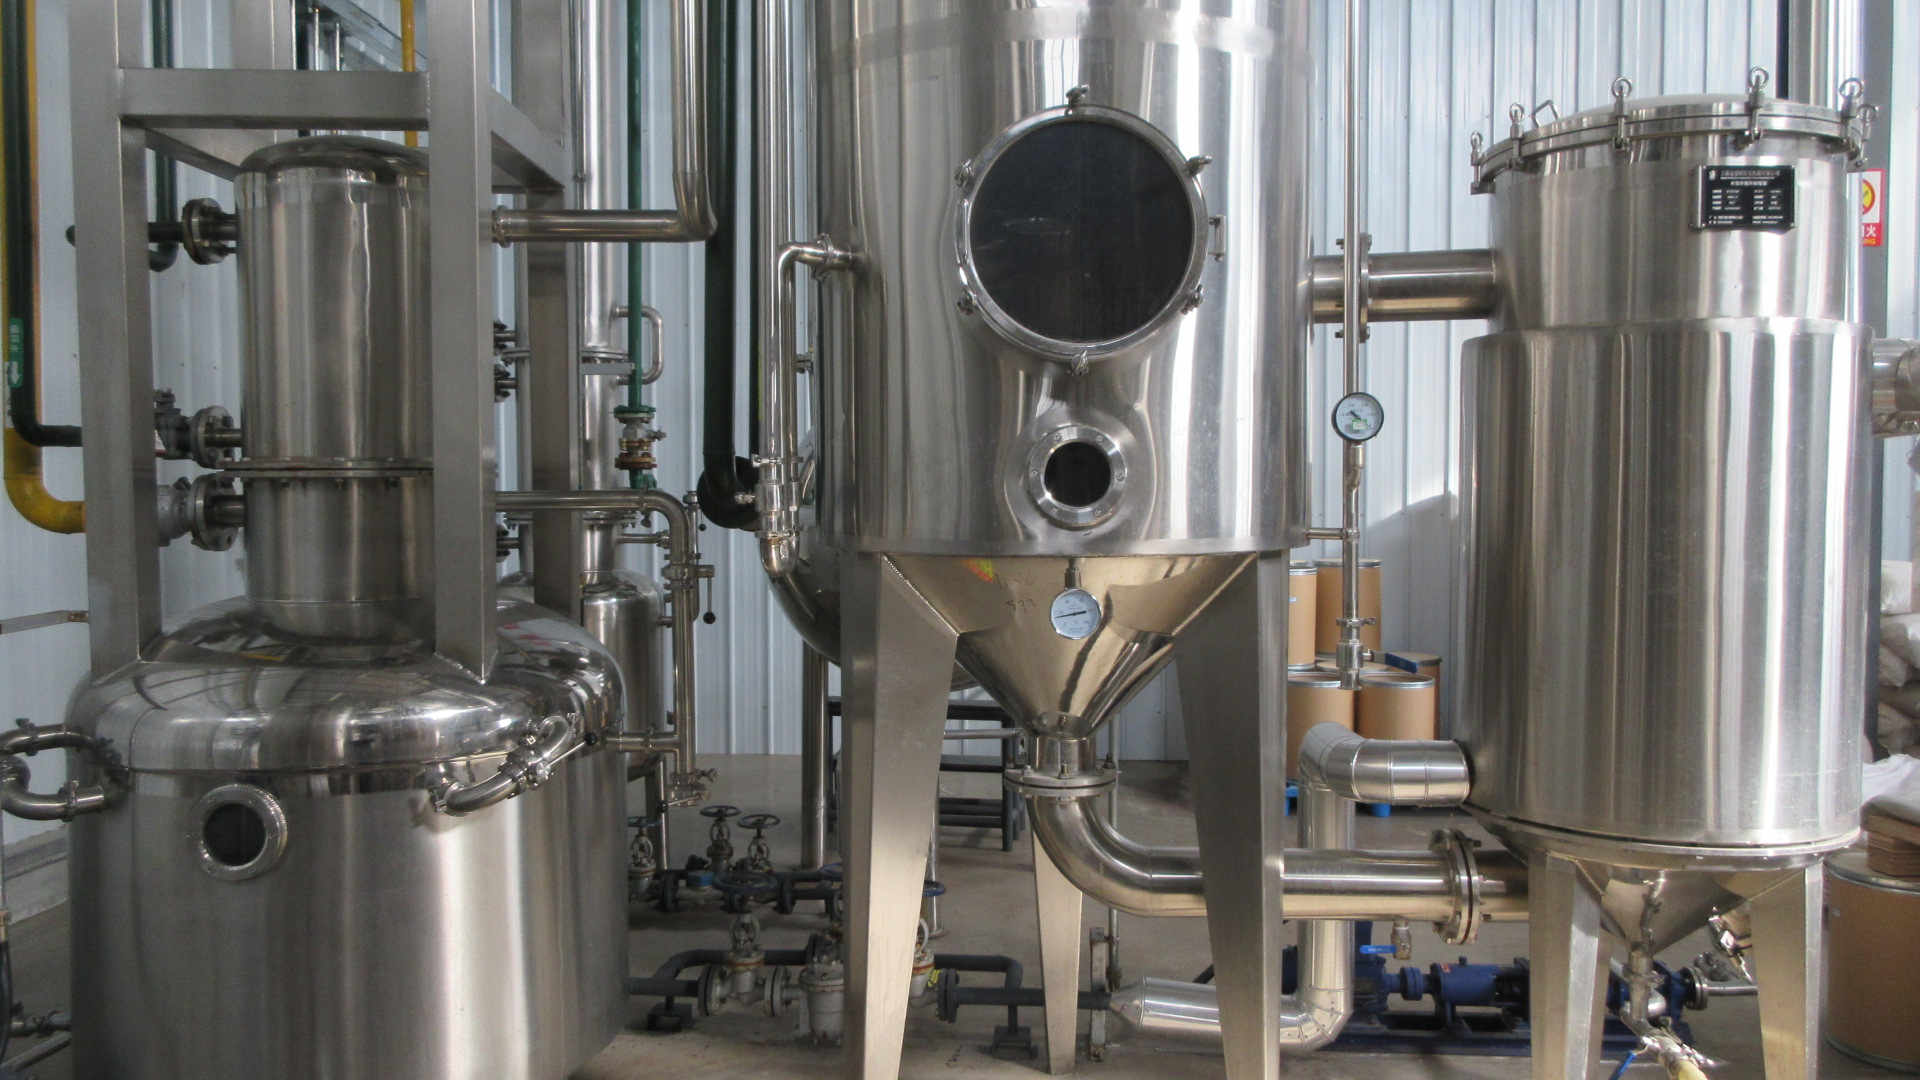
Vacuum Concentration
Low-temperature vacuum cycling prevents thermal degradation of heat-sensitive active compounds like sulforaphane, saponins, and ginsenosides.
 Step 03
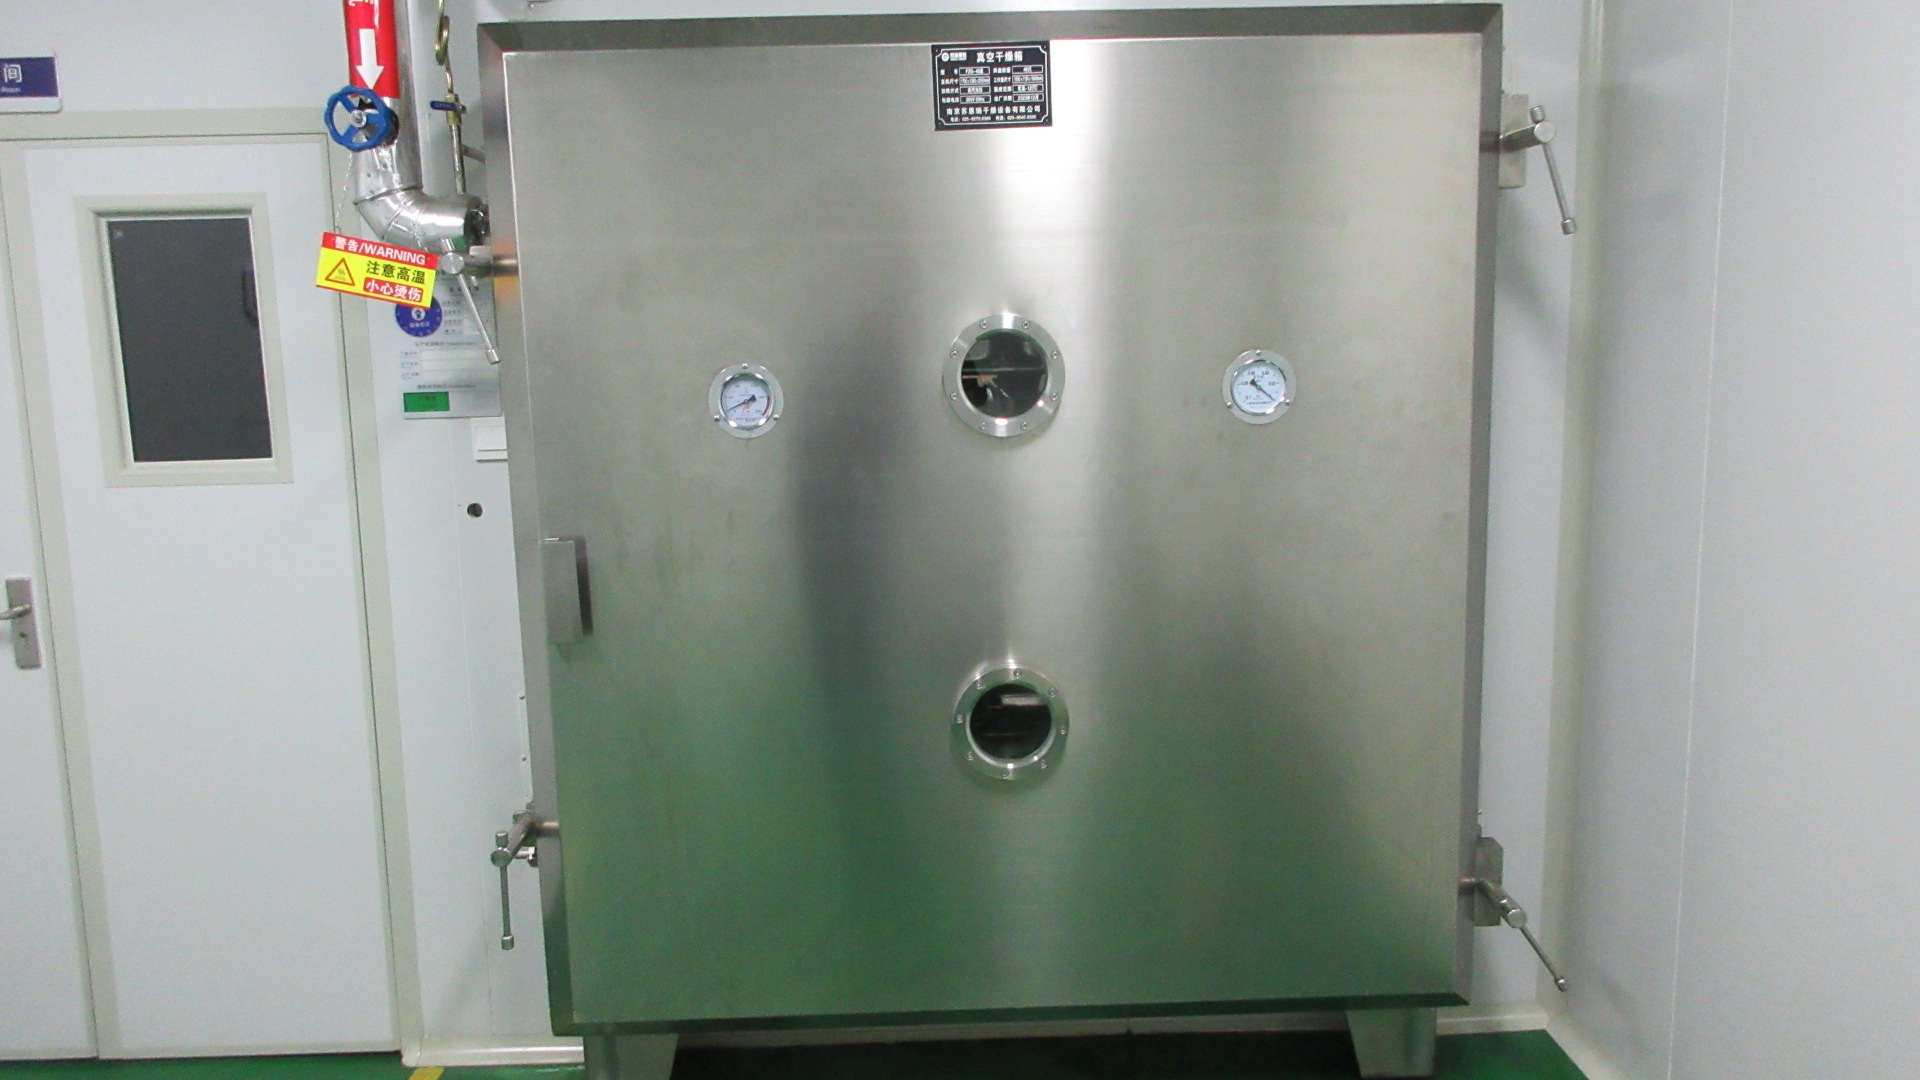
Spray & Vacuum Drying
Instant atomized spray drying converts concentrates into free-flowing, stable powders with verified residual moisture content under 5.0%.
 Step 04
Precision Smashing & Milling
Industrial micro-pulverizing mills crush products to specific granulations, ranging from 80-mesh standard powders to ultra-fine 200-mesh suspensions.
 Step 05
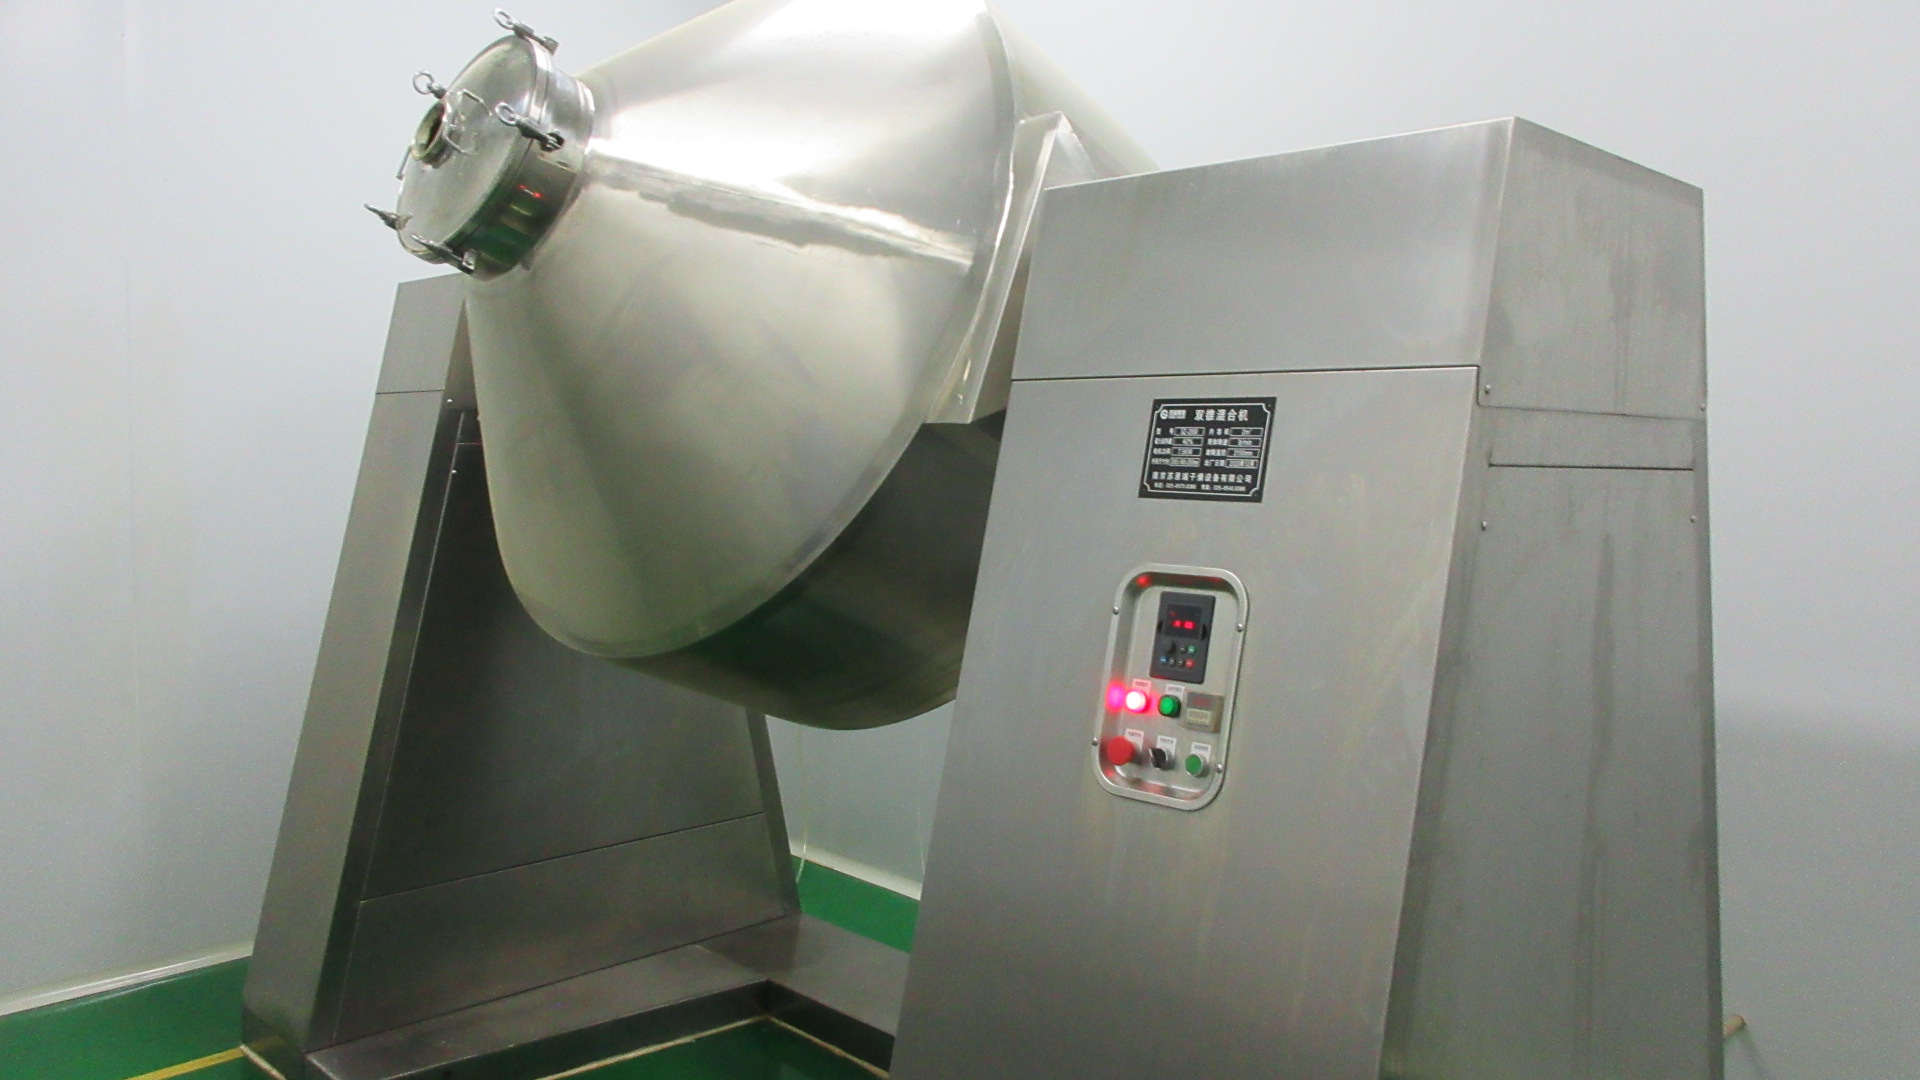
Homogeneous Mixing
High-capacity V-mixers and ribbon blenders ensure uniform distribution of active compounds across 500kg - 2,000kg single production batches.
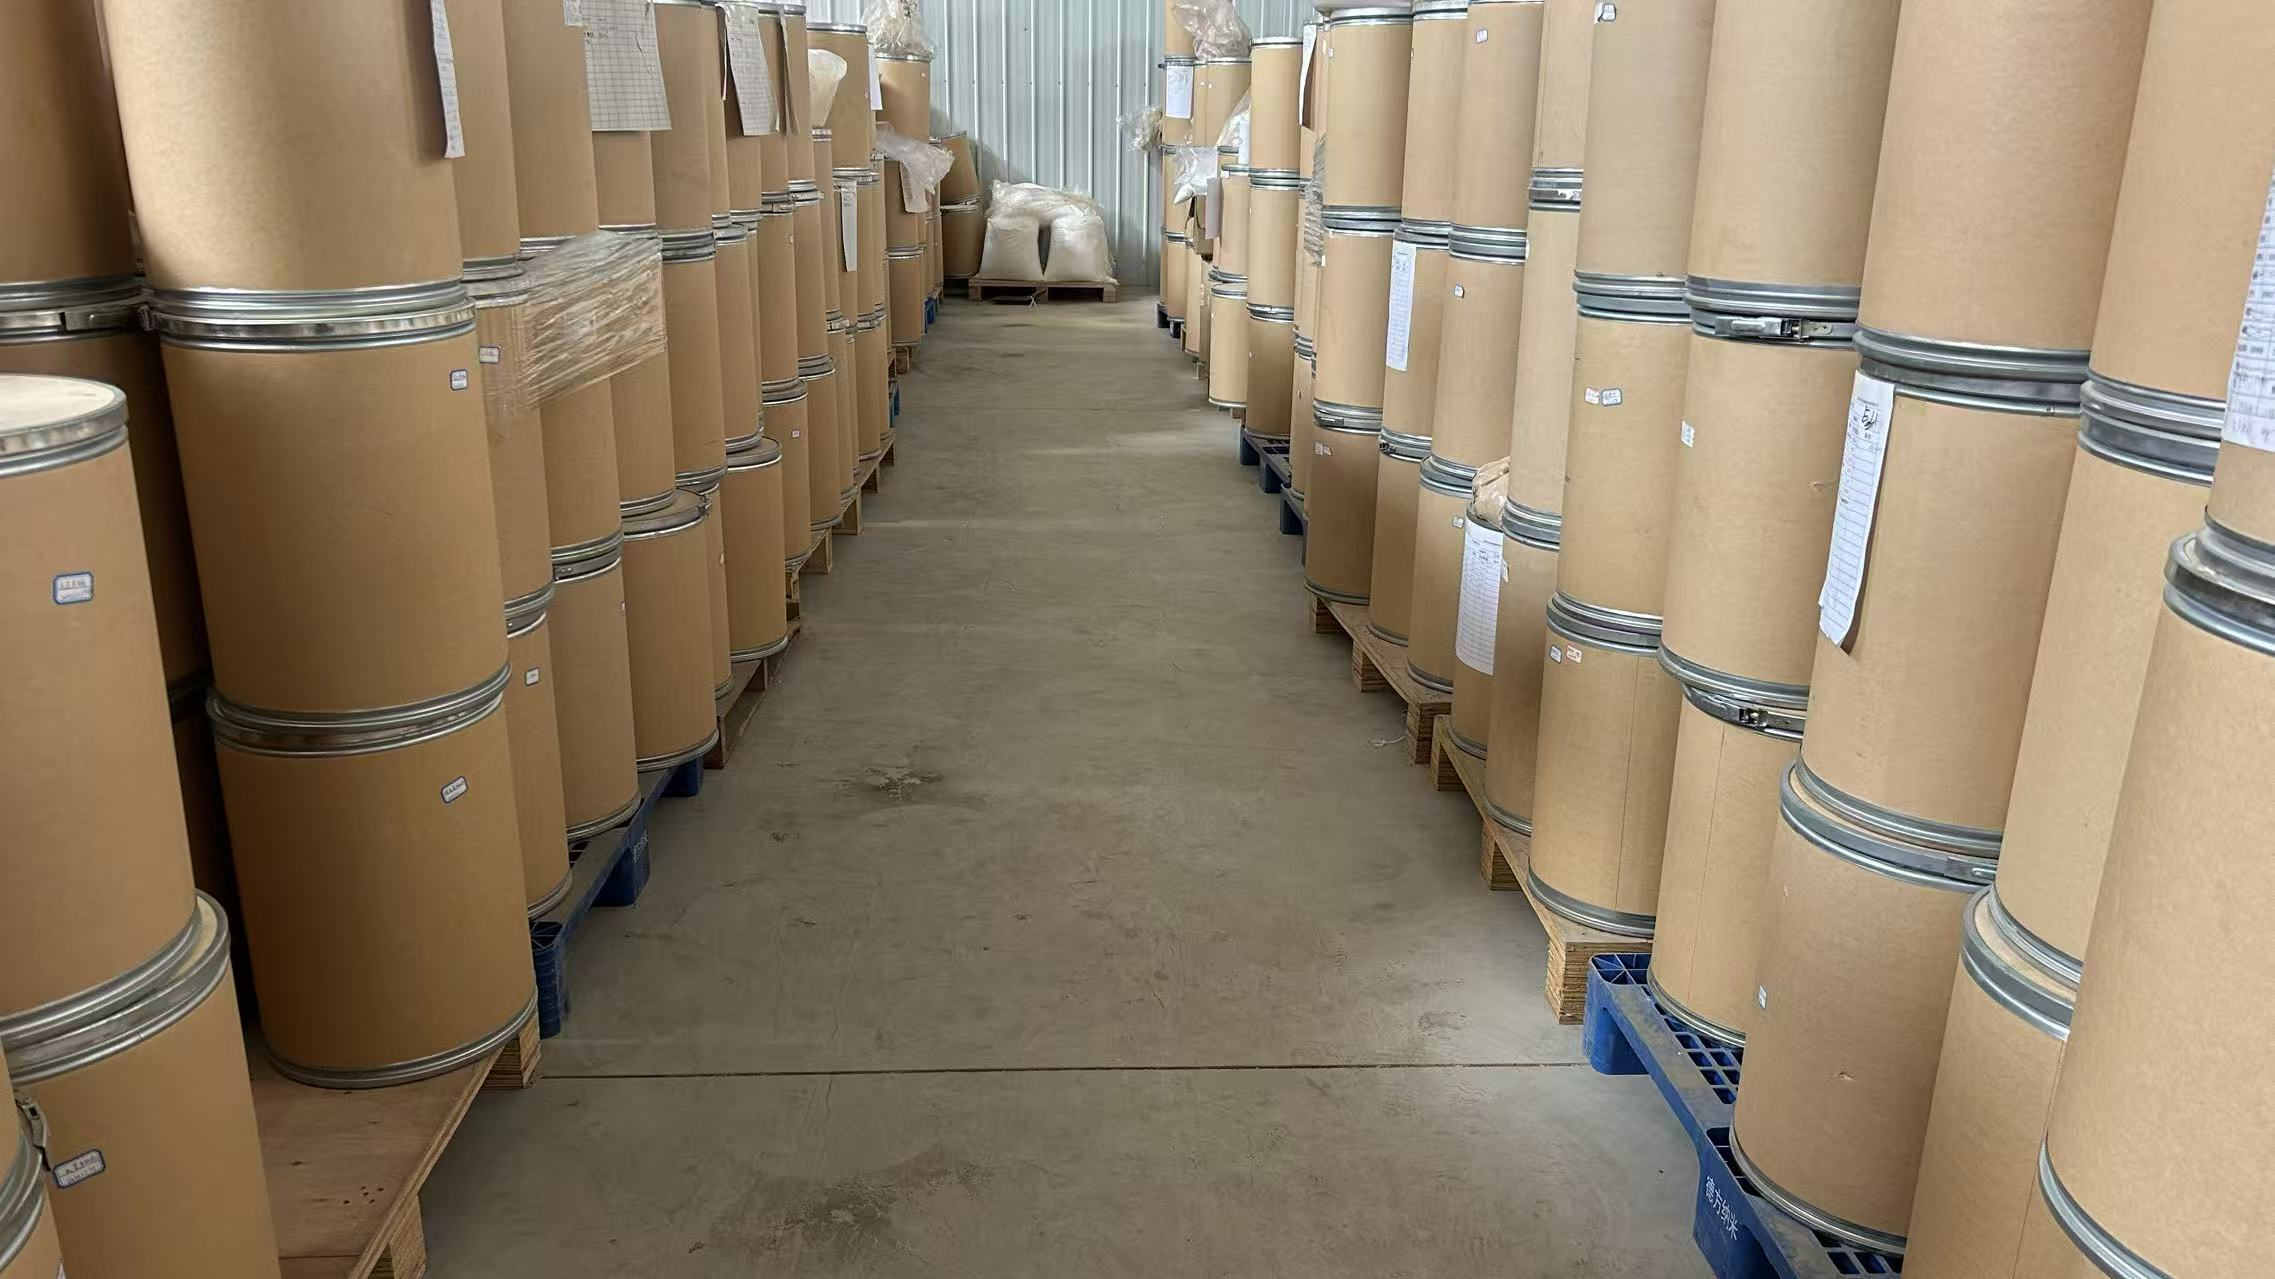 Step 06
QC Release & Vacuum Packing
Cleanroom packaging in pharmaceutical-grade food PE liners and double aluminum foil bags sealed within fiber drums, accompanied by batch COA.
Key Workshop Machinery & Equipment
Our infrastructure includes 6 core equipment categories configured for industrial scale, safety compliance, and continuous batch traceability.
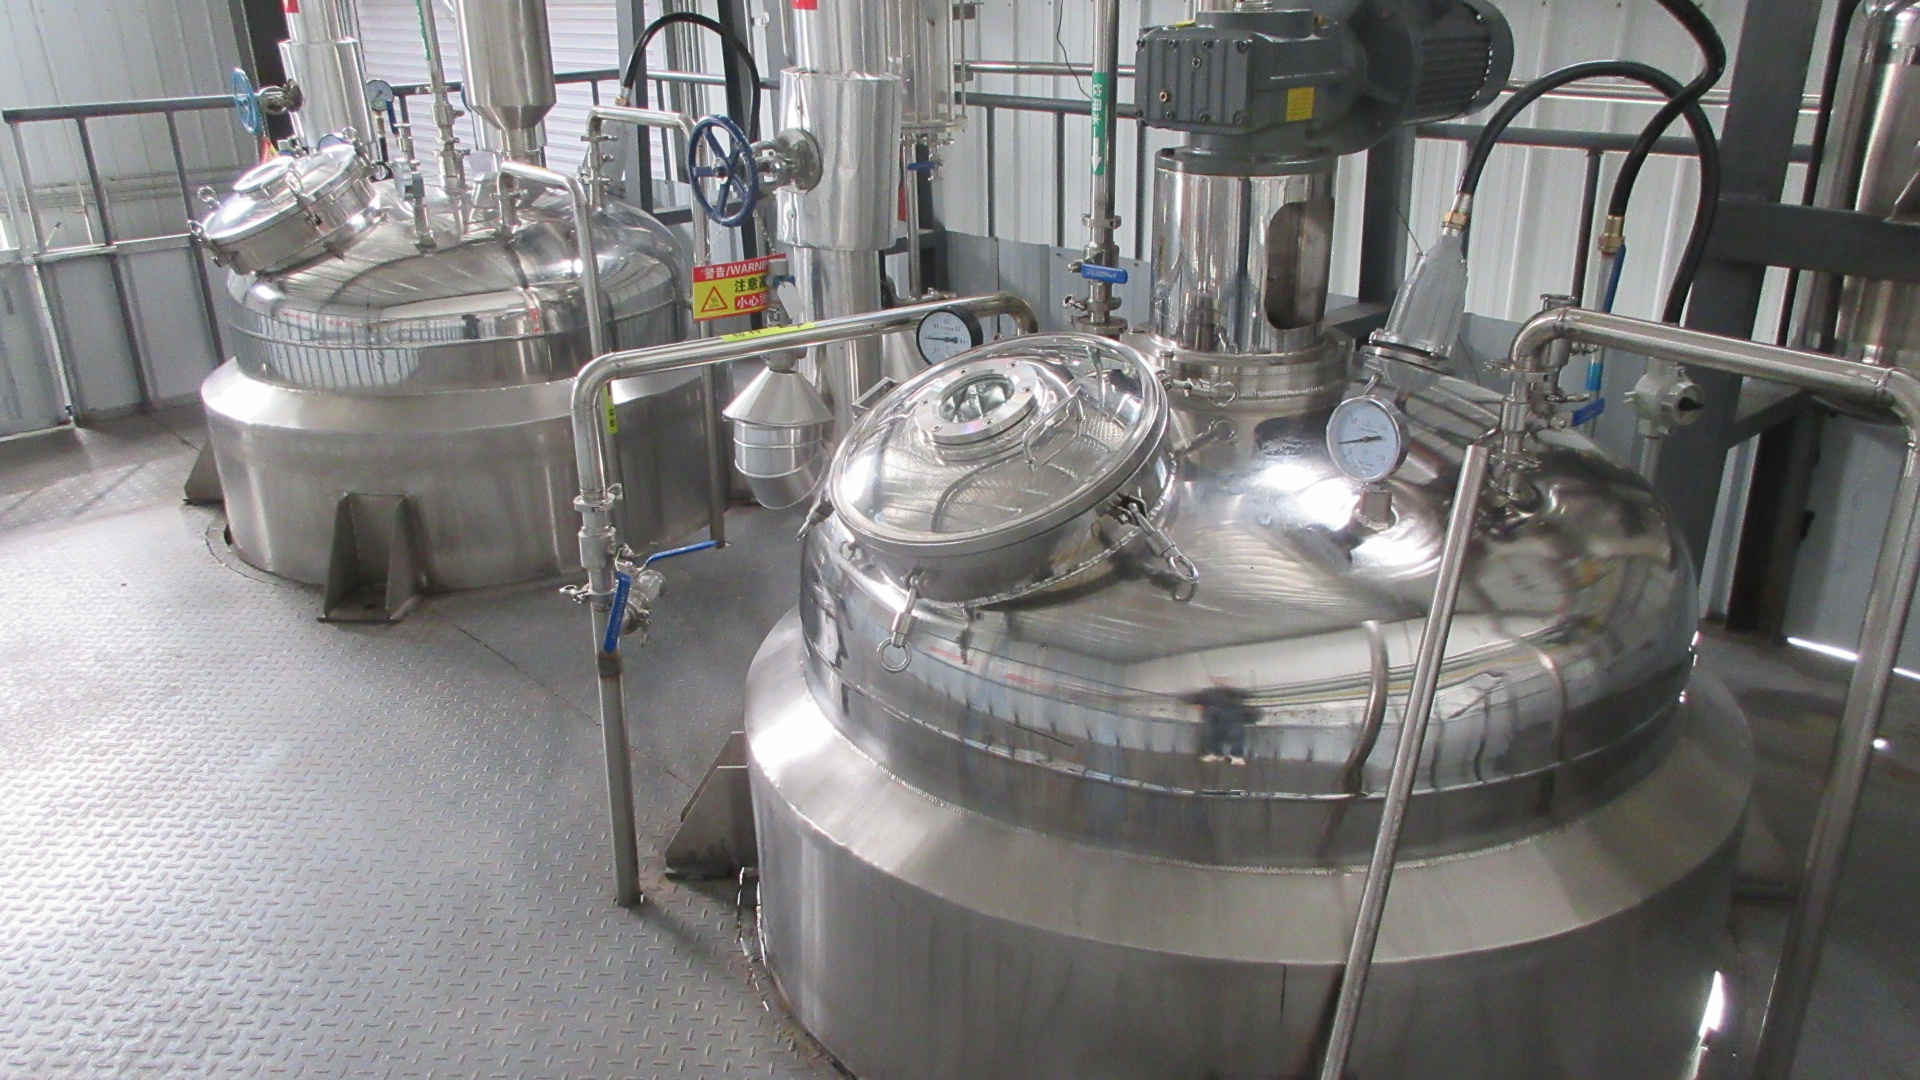
Stainless Extraction Tank
Dual-solvent multi-functional extractor with dynamic cycling and reflux condensers.
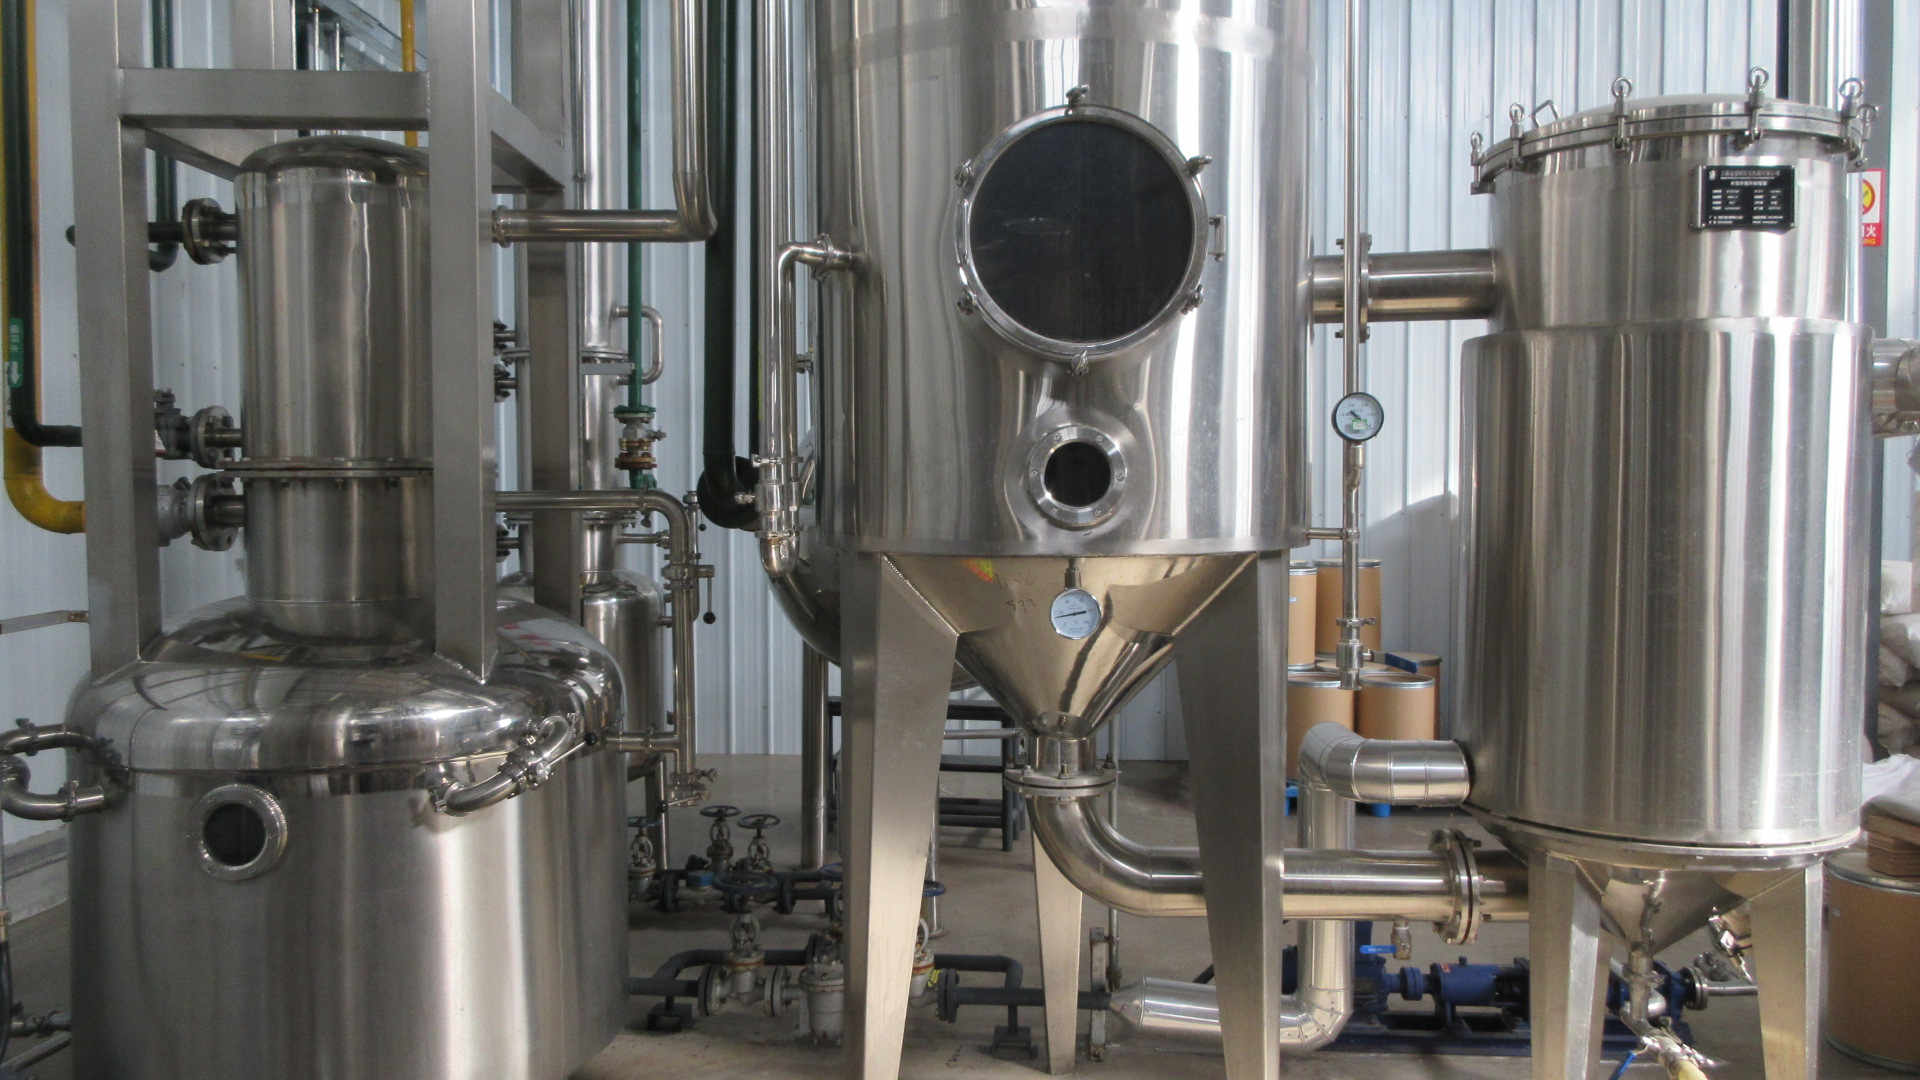
Concentrating Tank
Spherical low-temperature vacuum concentrator engineered for heat-sensitive actives.
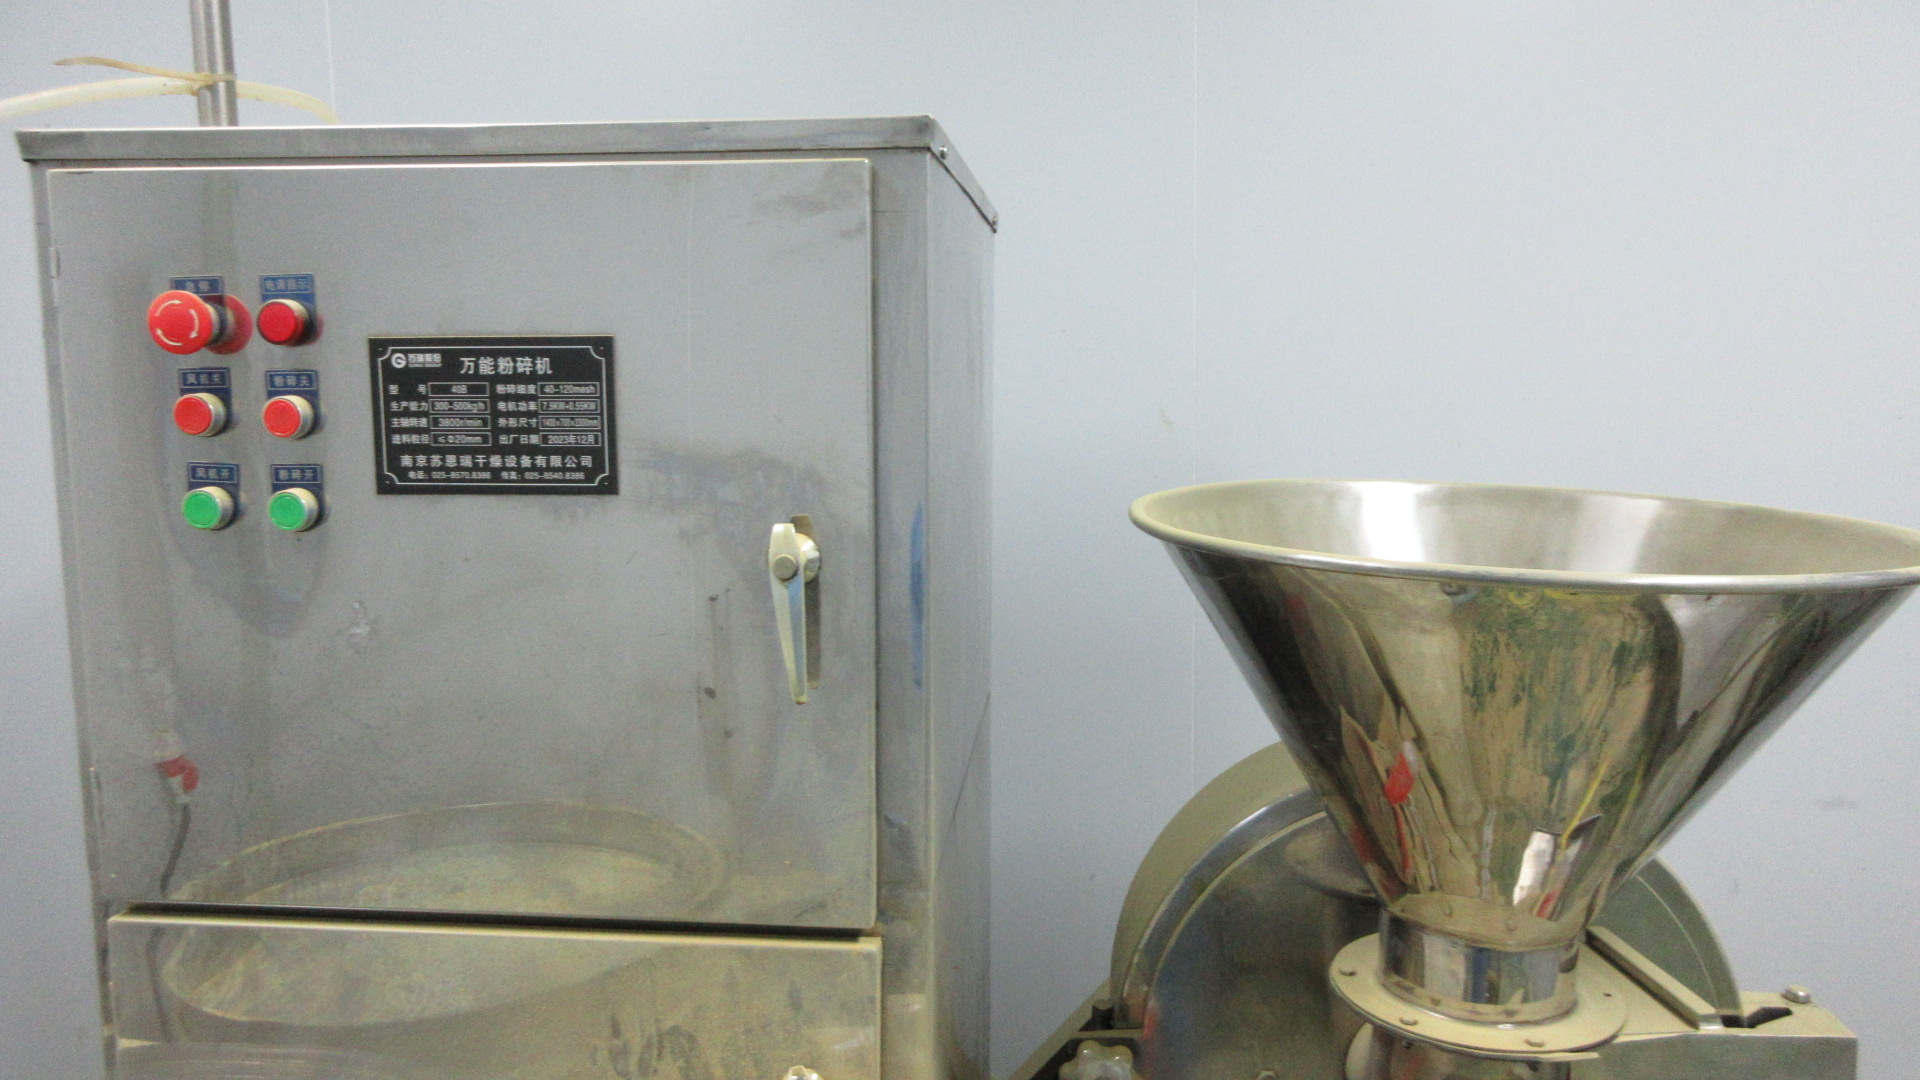
Smash & Milling Machine
High-speed mechanical pulverizer with pneumatic sieving to ensure uniform particle size.
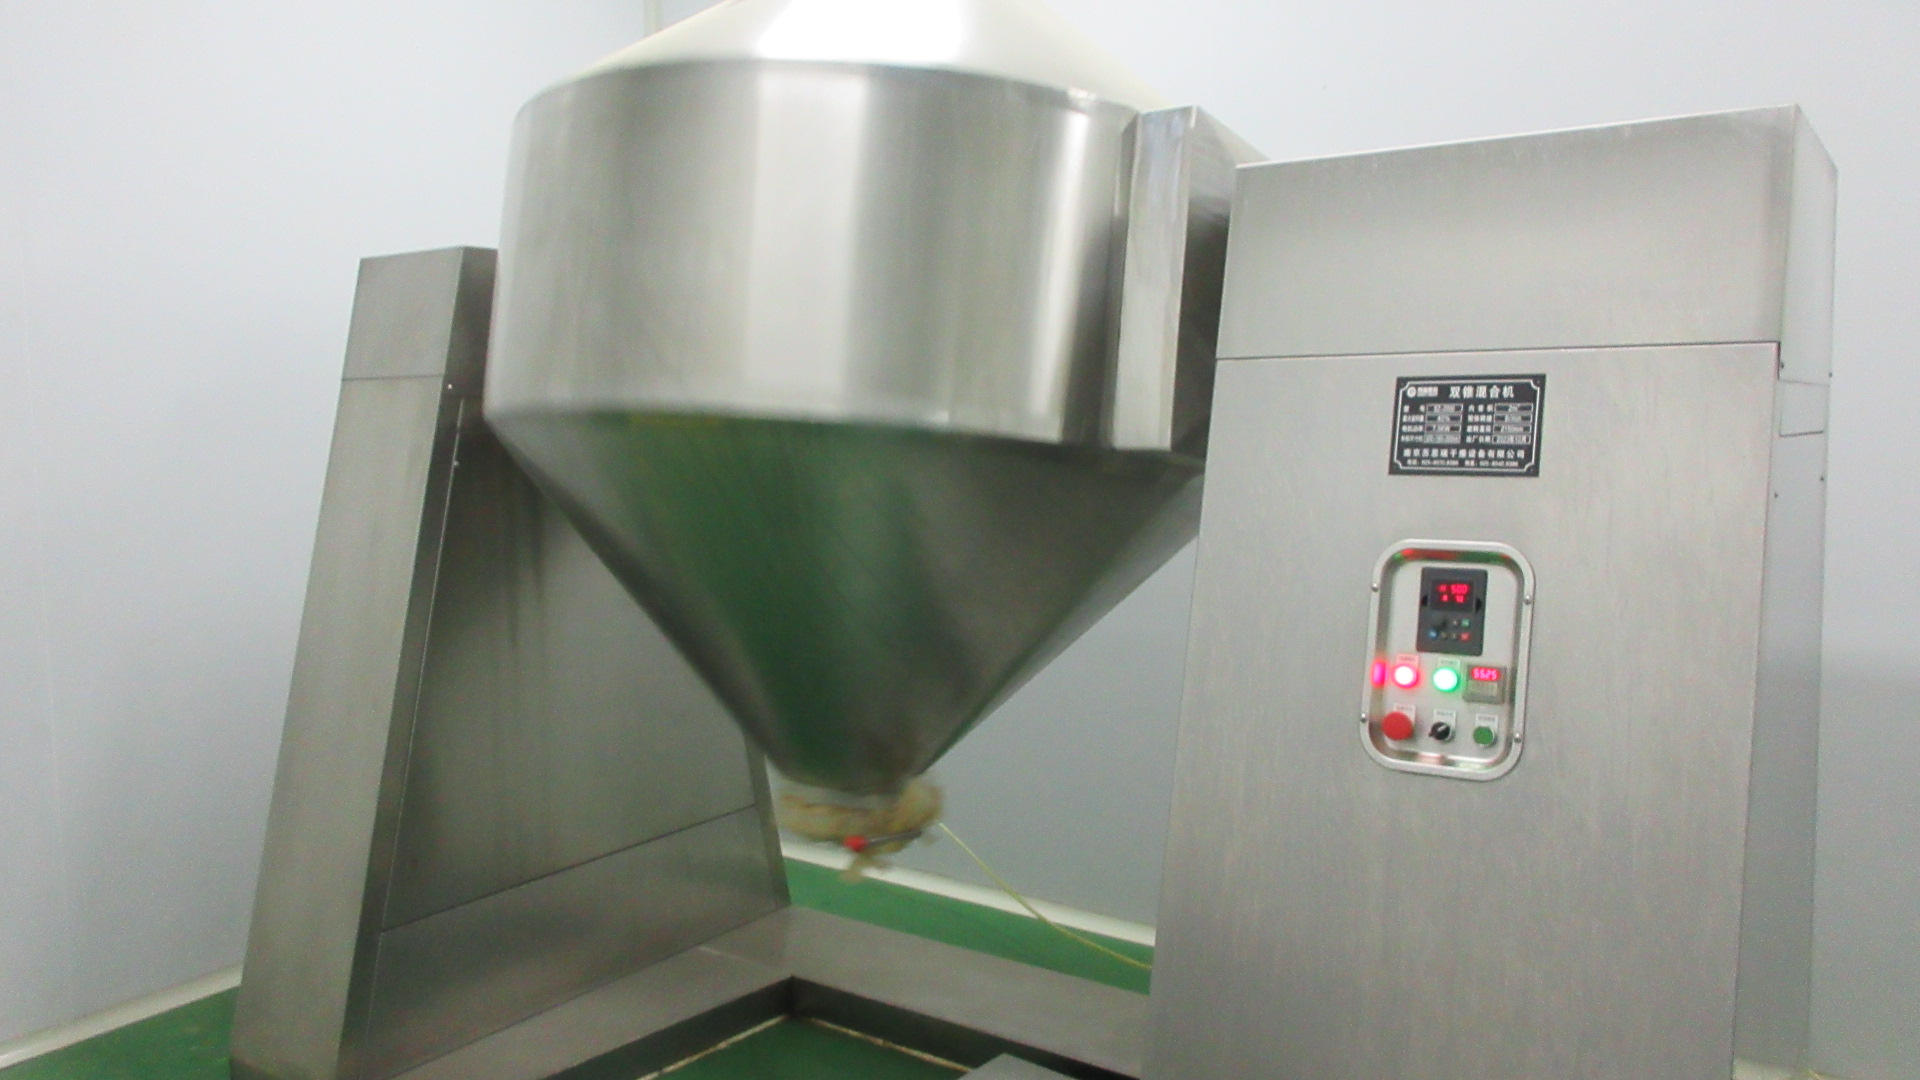
Rotary Powder Mixer
3D motion blender supporting custom formula premixes, uniform coloring, and excipients.
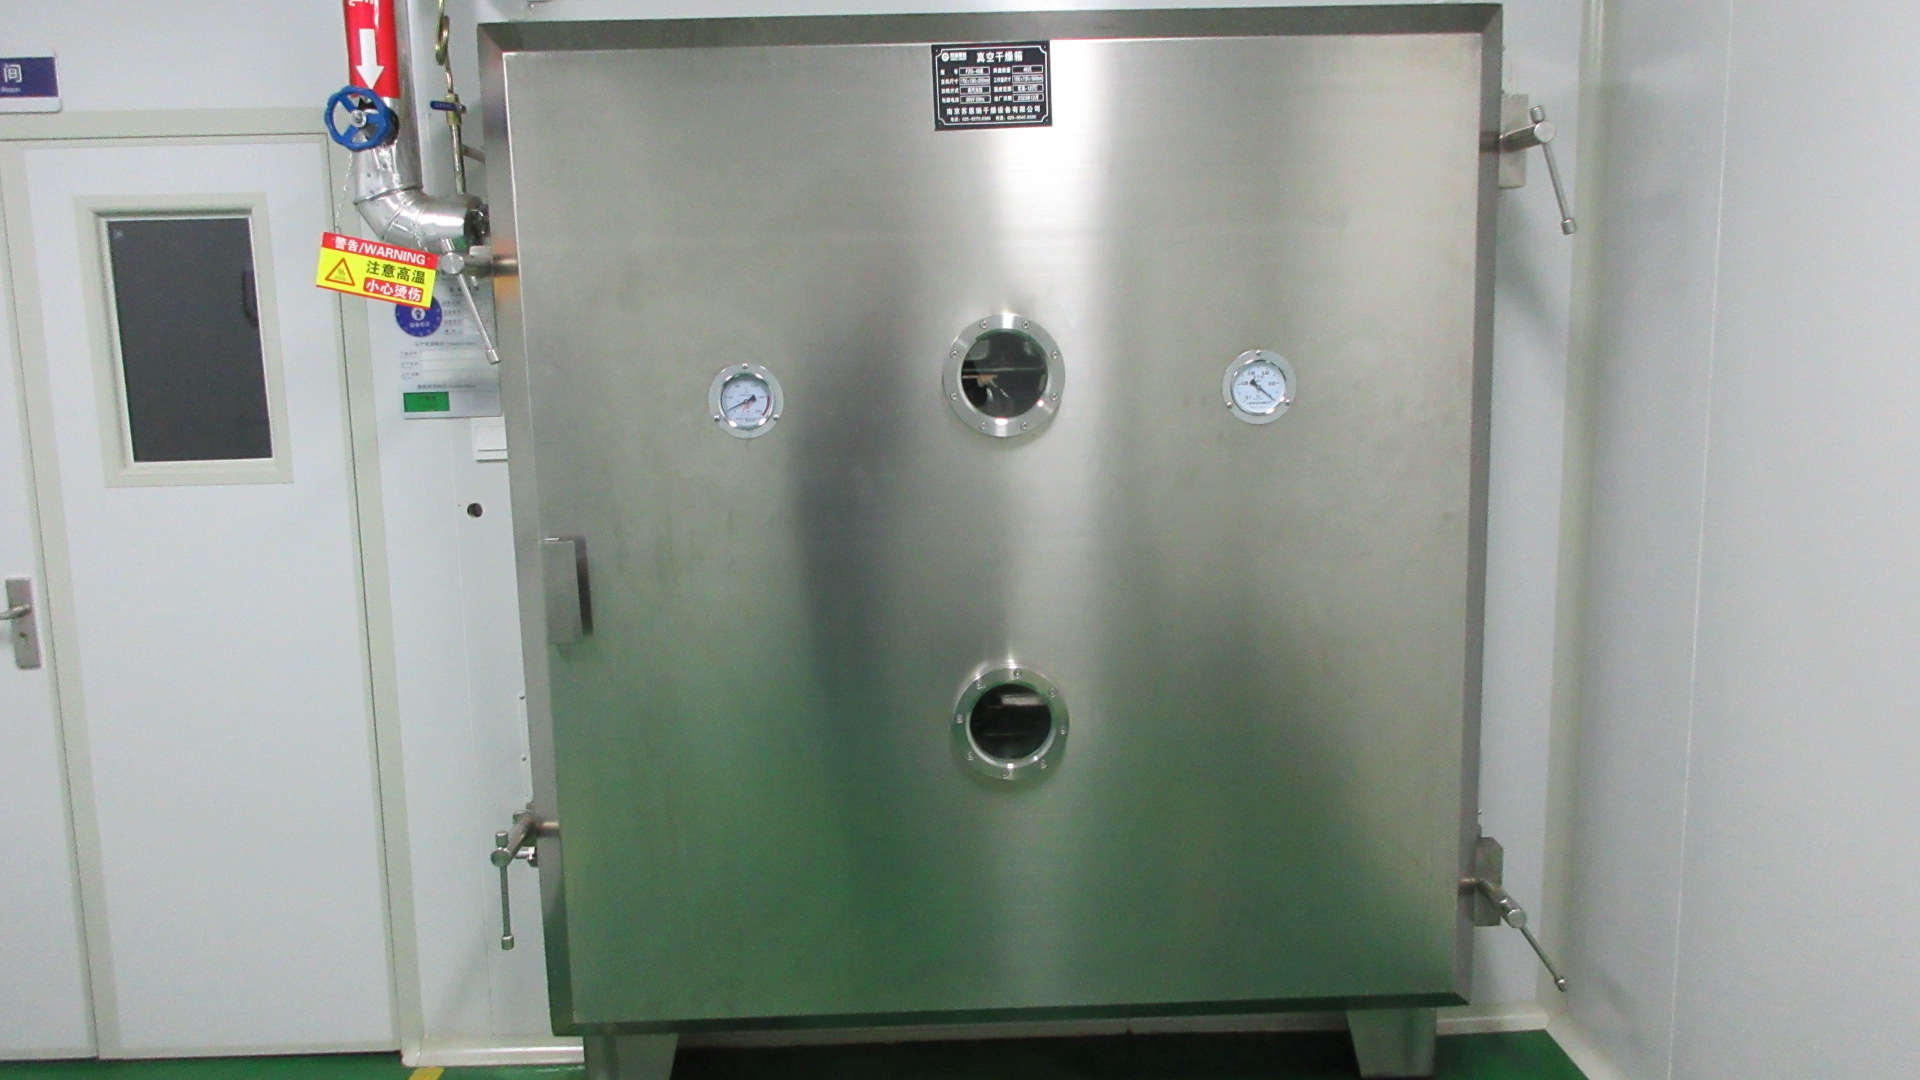
Hot Air Circulation Oven
Precision thermostatic drying chamber for granular ingredients and moisture adjustment.
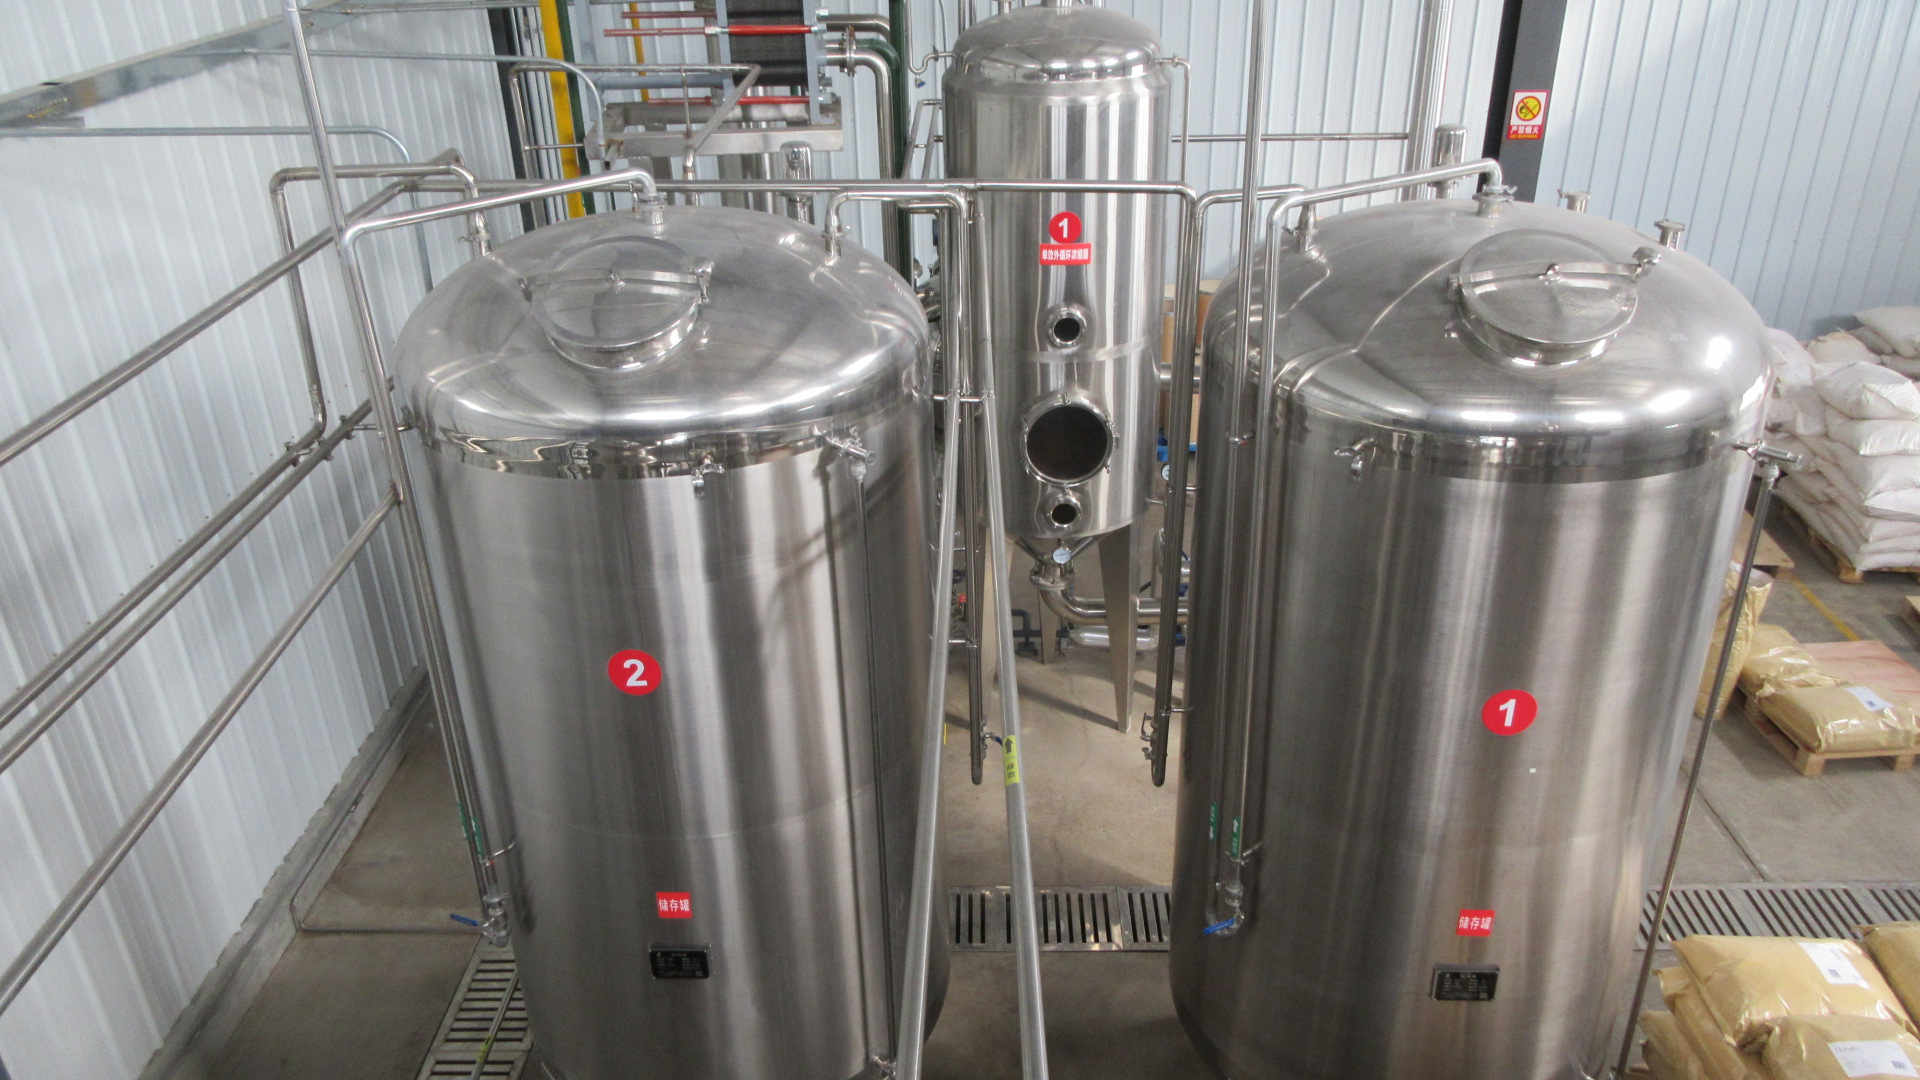
Sealed Storage Tank
Sanitary intermediate holding tank ensuring contamination-free fluid transfers.
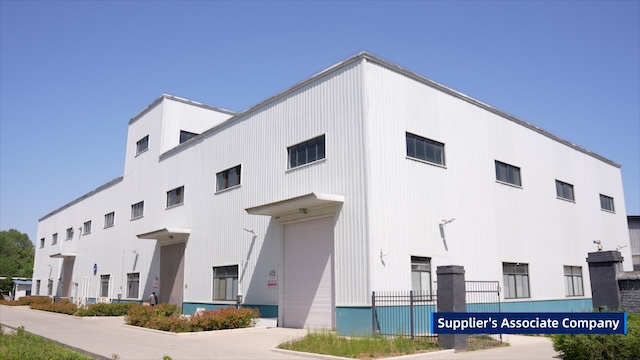
Production Workshop
Enclosed, climate-managed plant layout organized according to ISO 22000 hygiene flow.
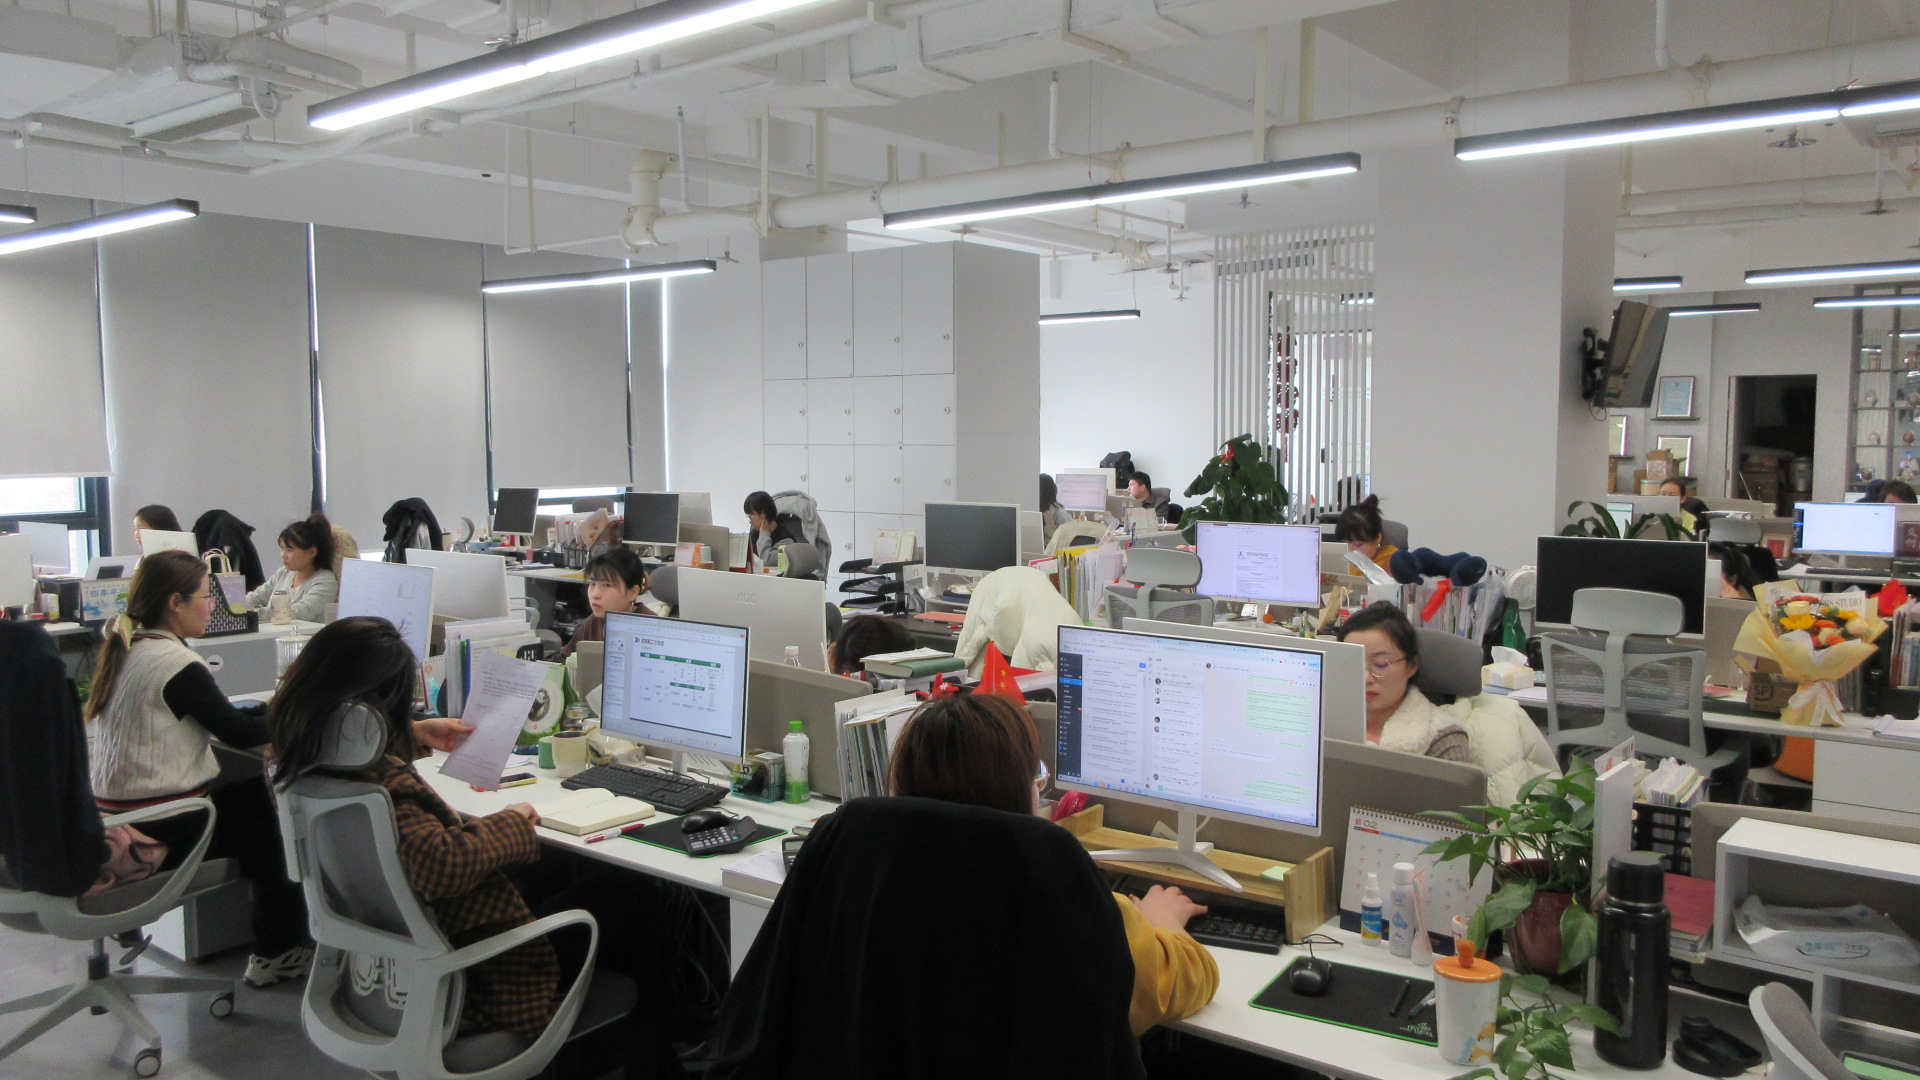
Packaging Line
Sealed drum filling and vacuum pouch sealing station under positive-pressure air filtration.
Analytical Quality Control & Testing Facility
No lot is released without documented testing. Our 3 dedicated QA/QC chemists and 4 R&D engineers cross-verify marker assays, physical traits, heavy metals, and microbes.
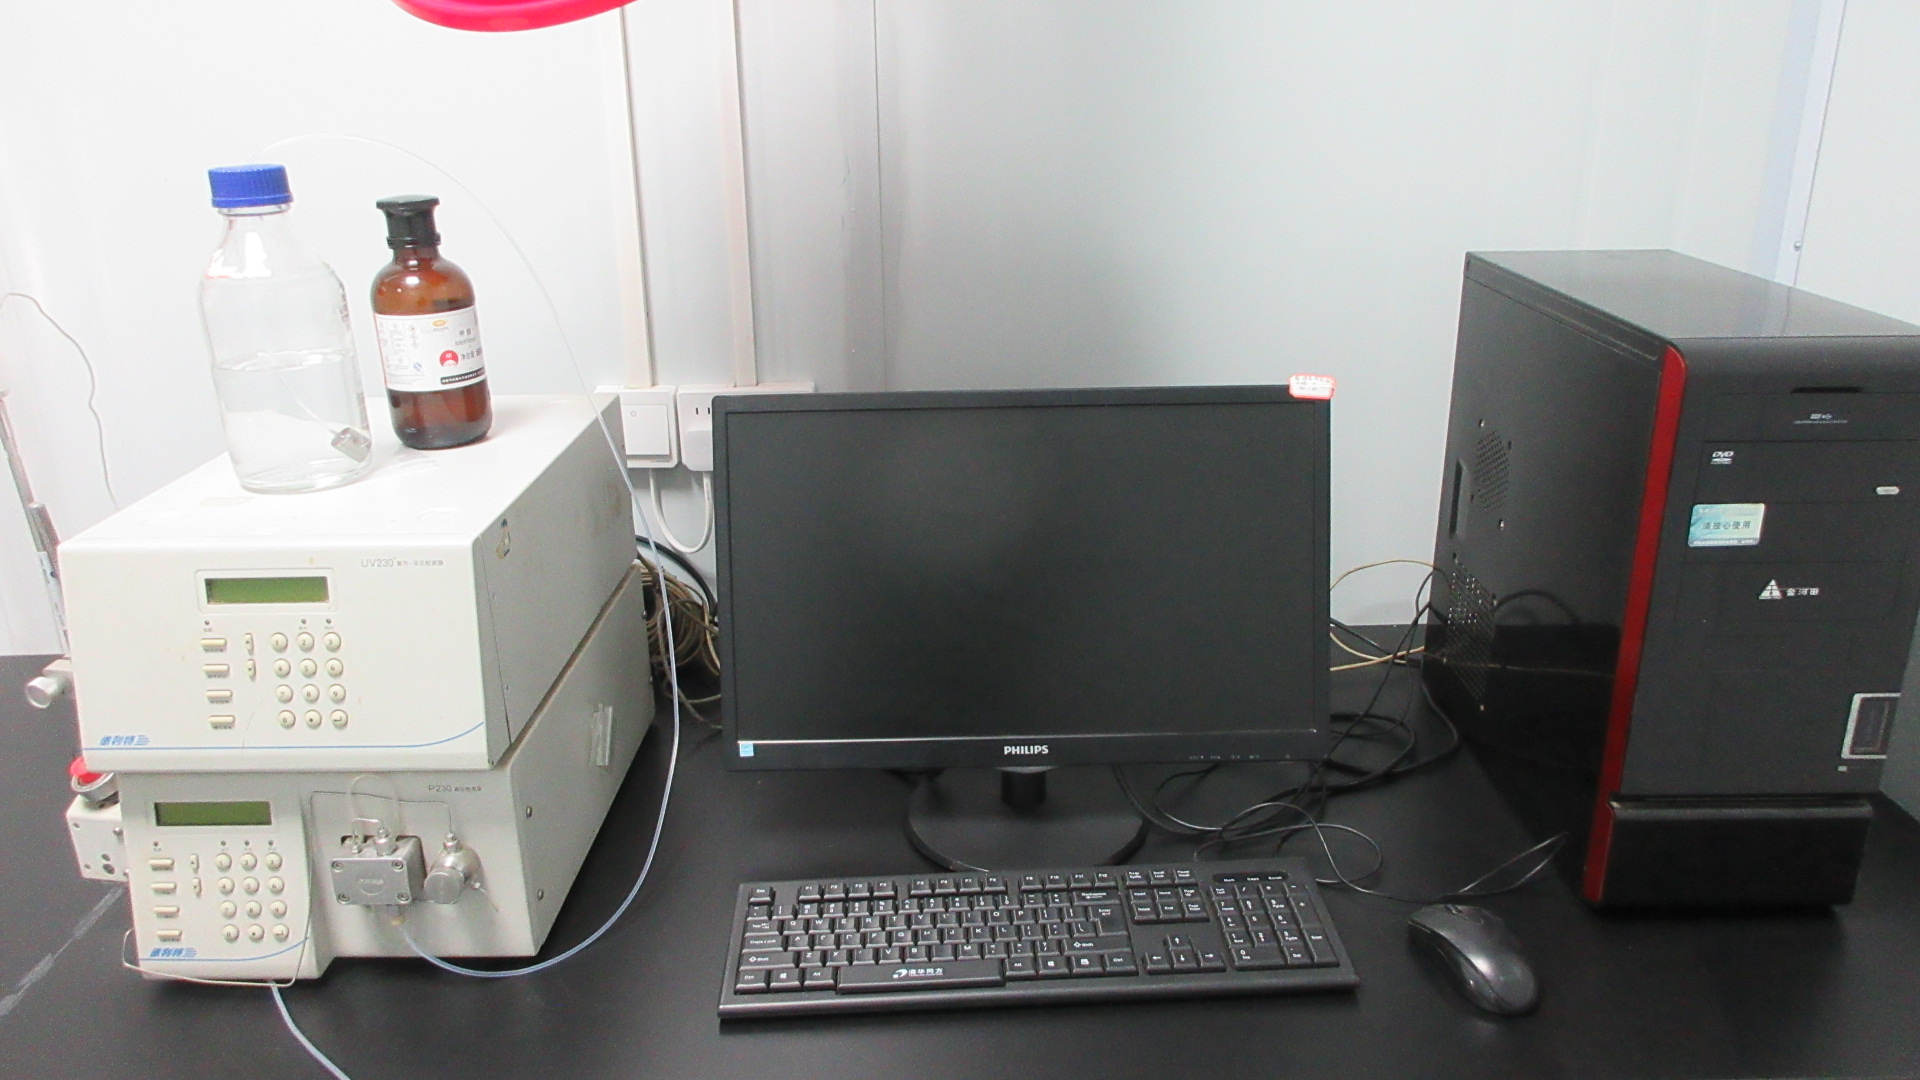
HPLC Analysis Unit 01
Quantifies active marker concentrations against USP/EP reference standards.
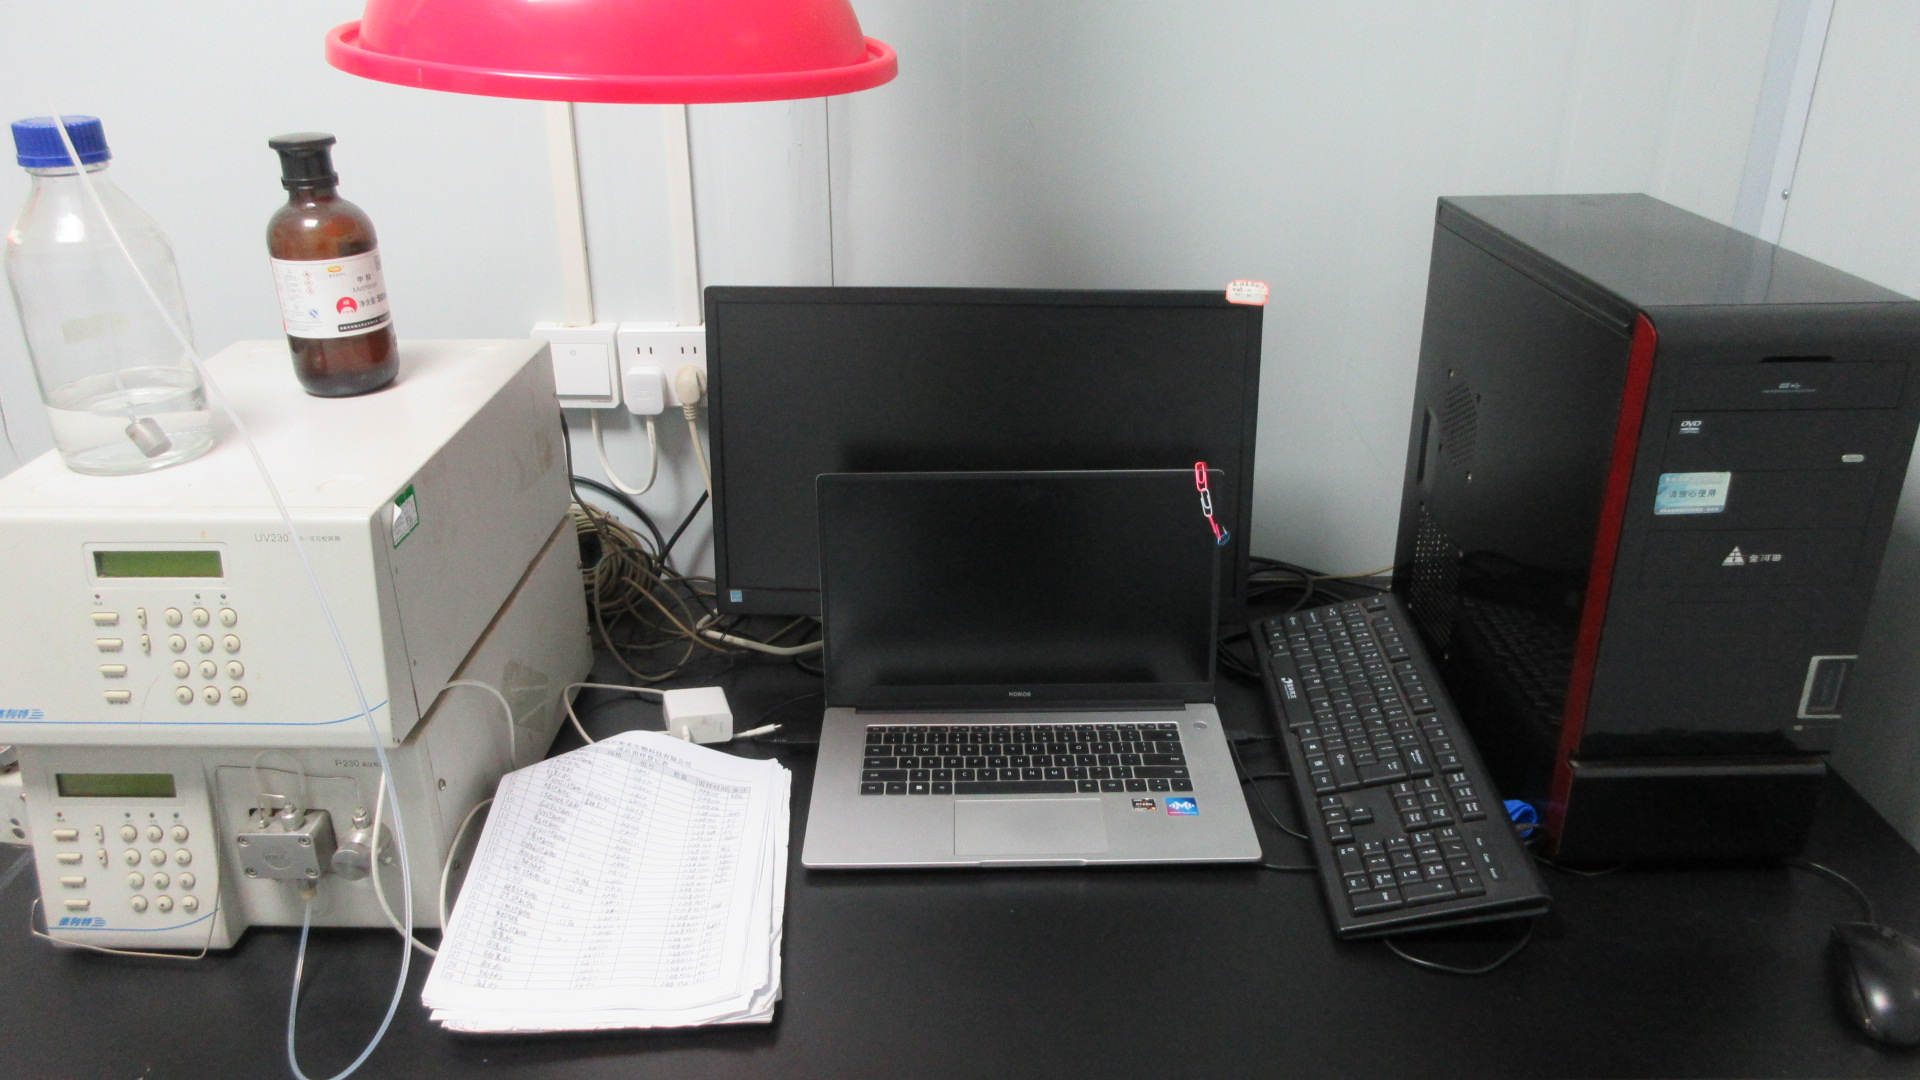
HPLC Unit 02 (R&D)
Dedicated to method development, solvent residue scans, and stability profiling.
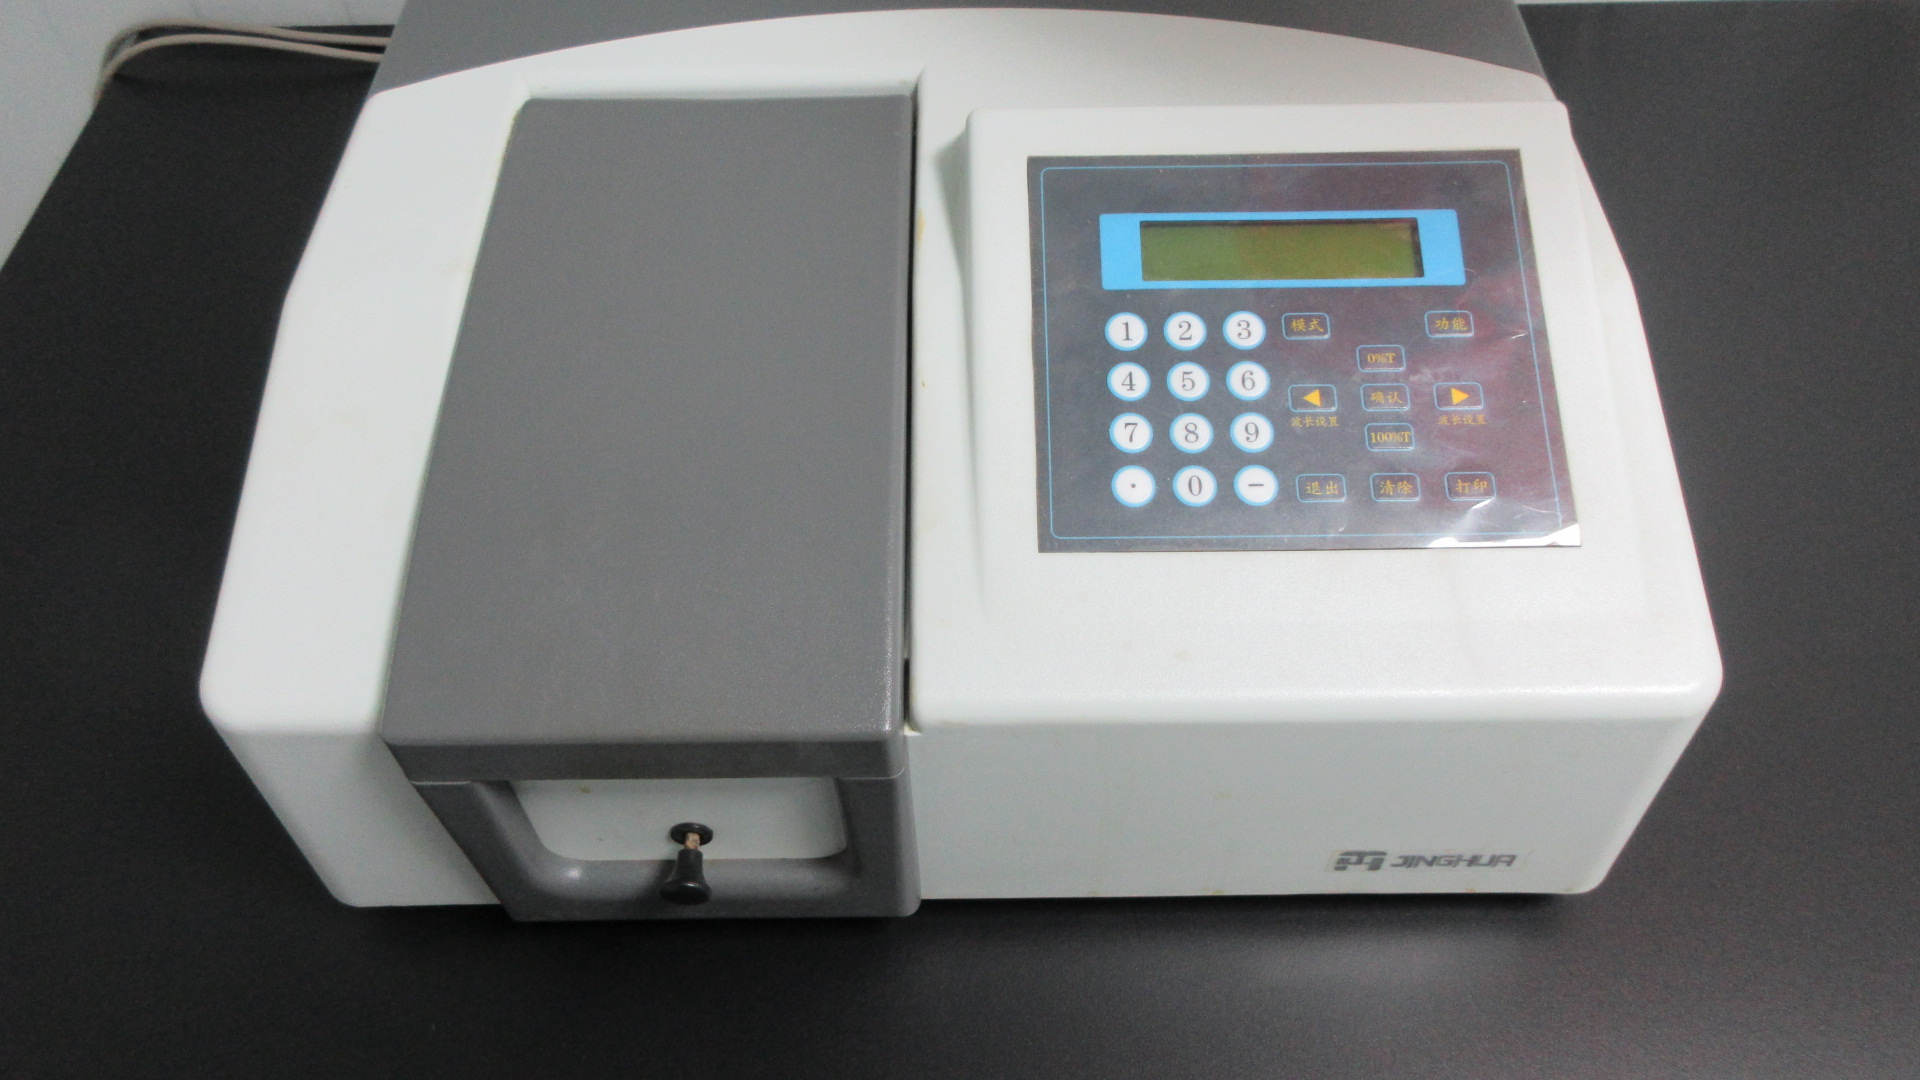
UV Spectrophotometer
Assays total polyphenols, polysaccharides, and colorimetric index curves.
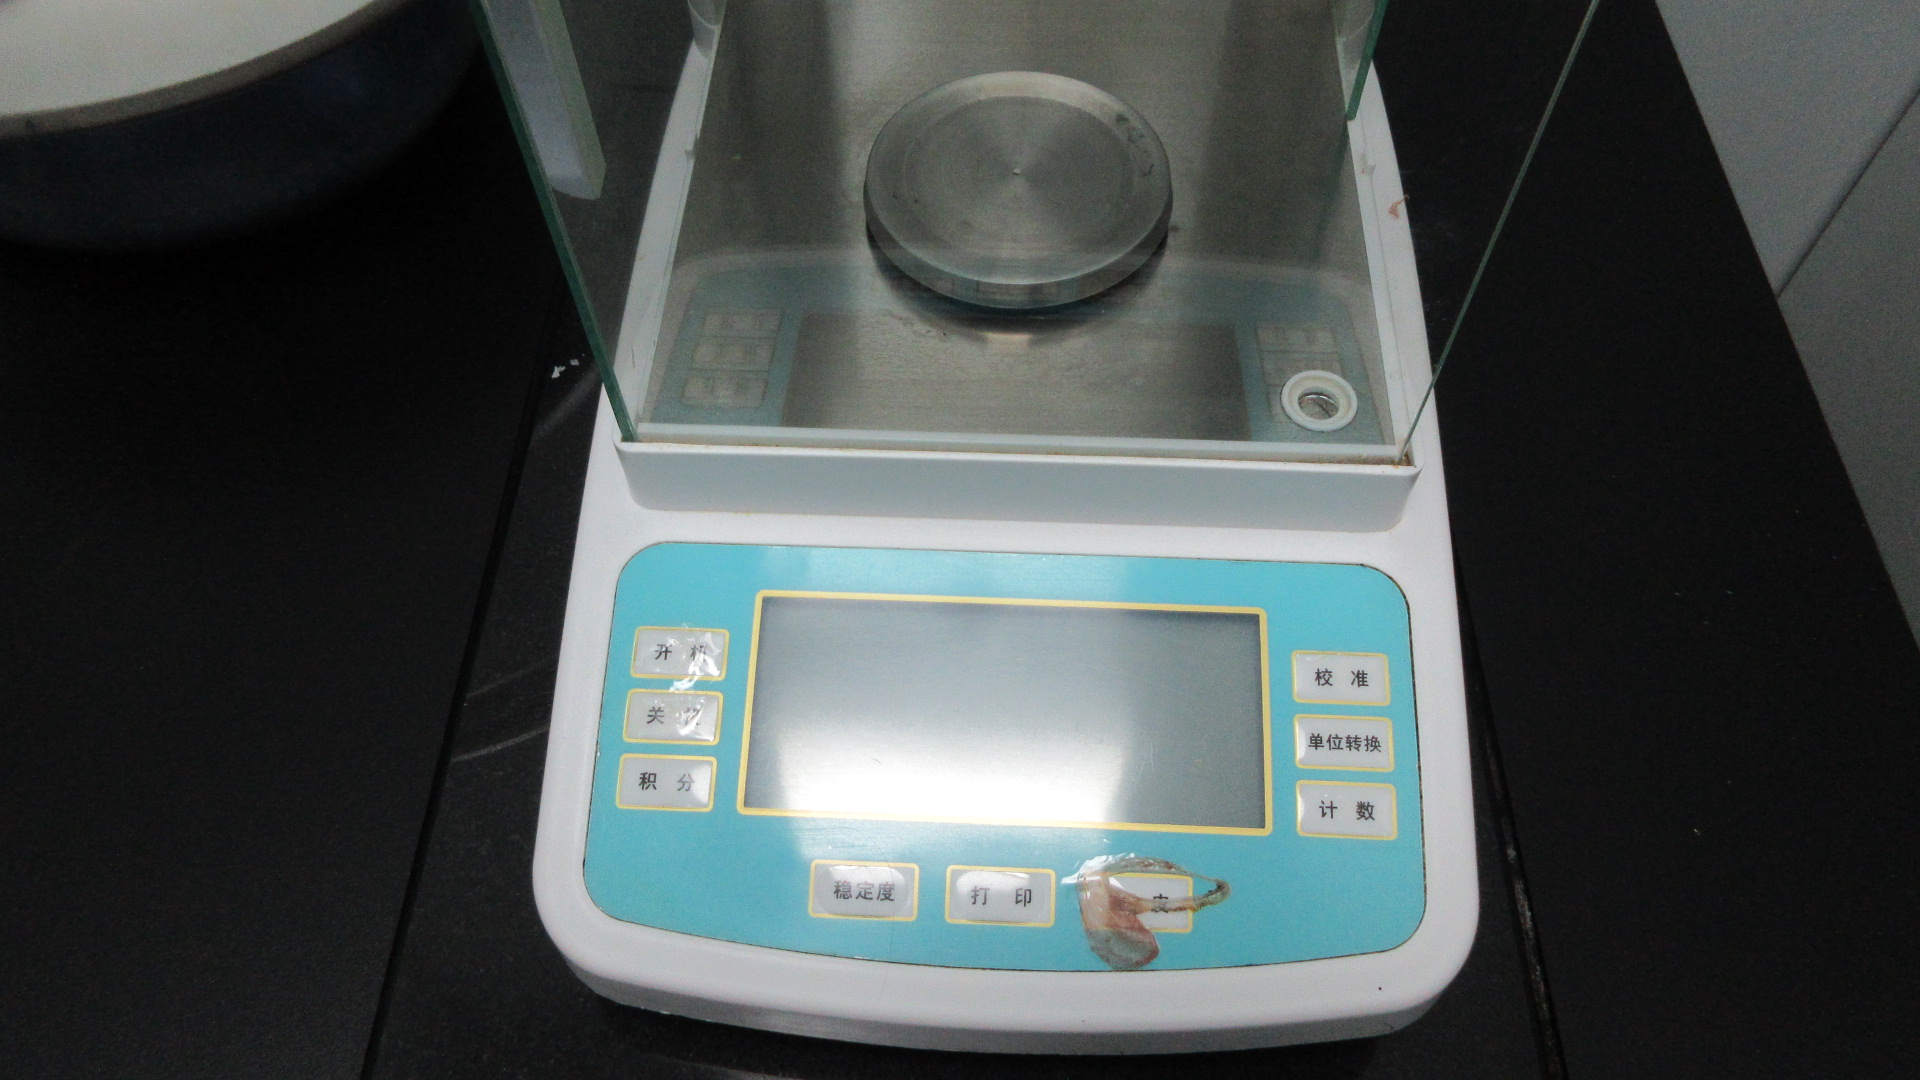
Analytical Micro-Balance
0.0001g high-precision weighing balance for primary standard preparation.
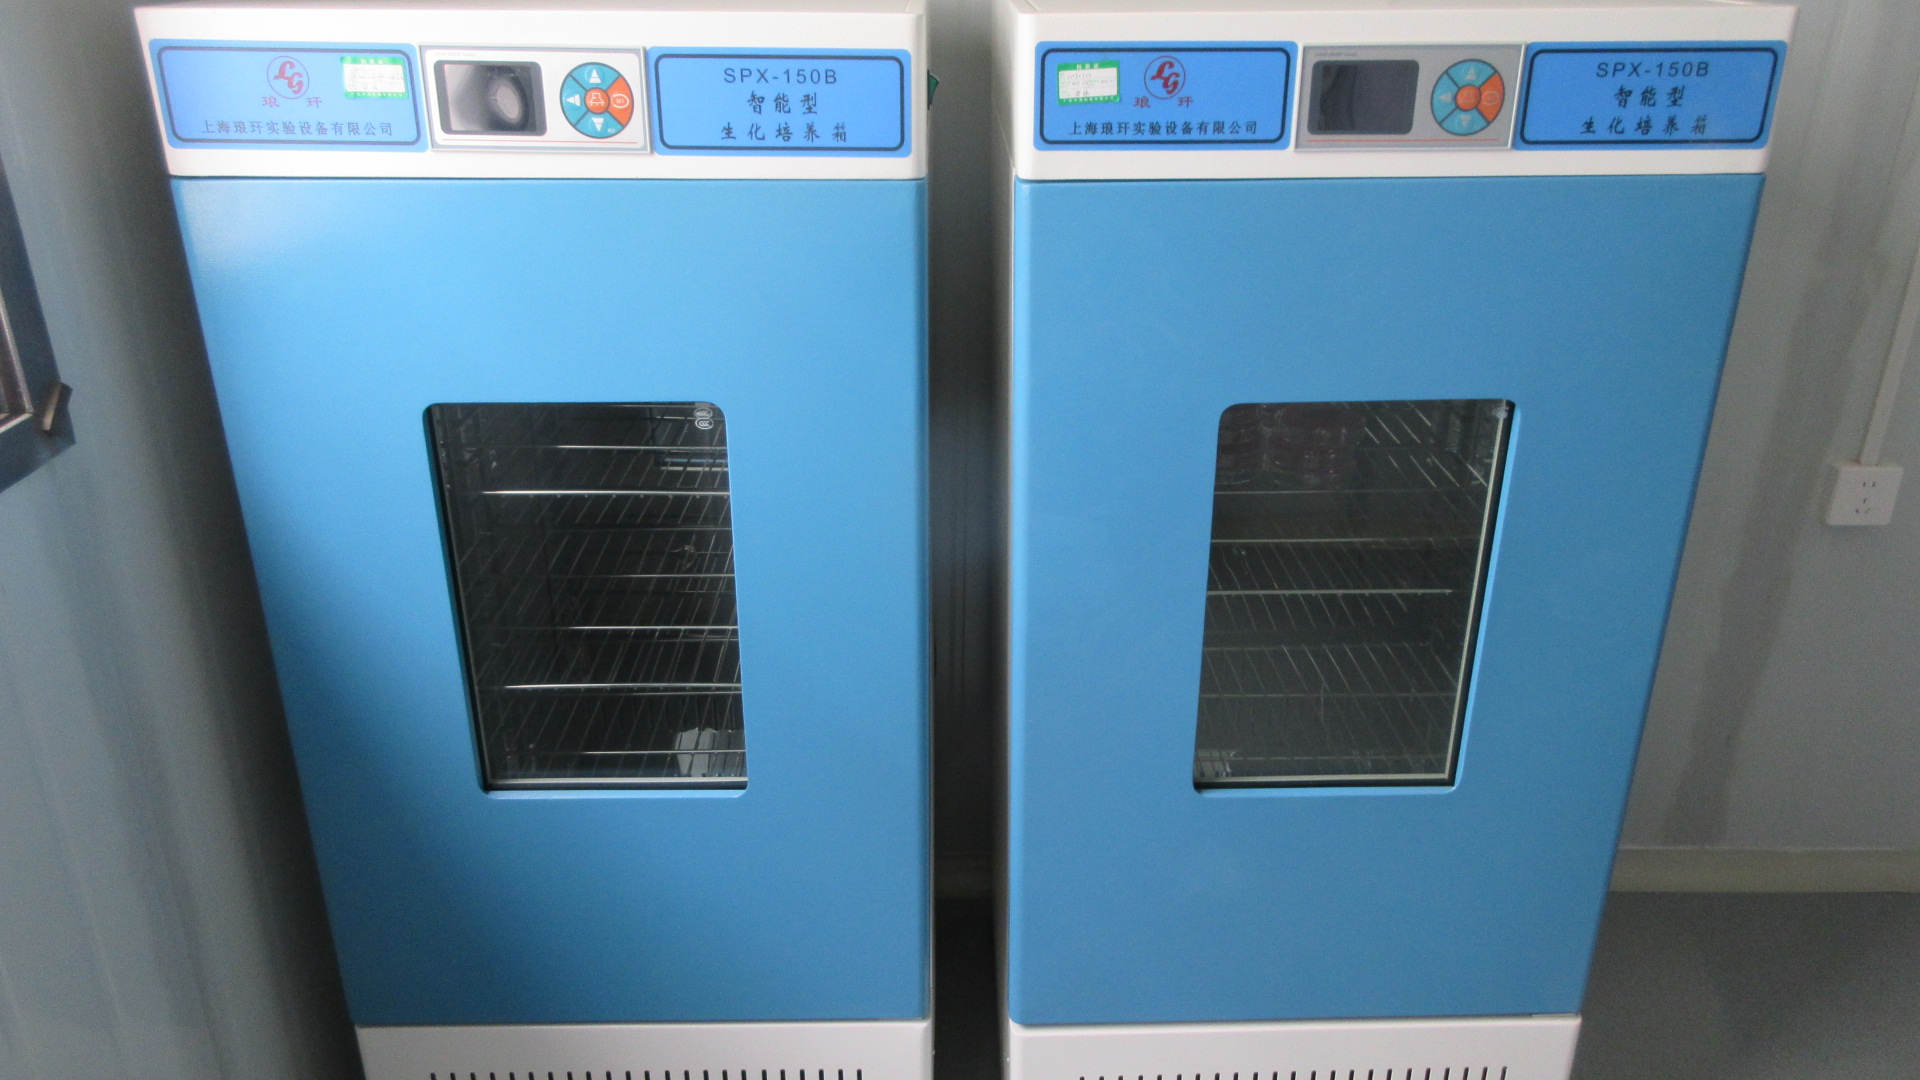
Constant Temp Incubator
Aerobic plate counts, yeast, mold, and pathogenic microorganism incubation.
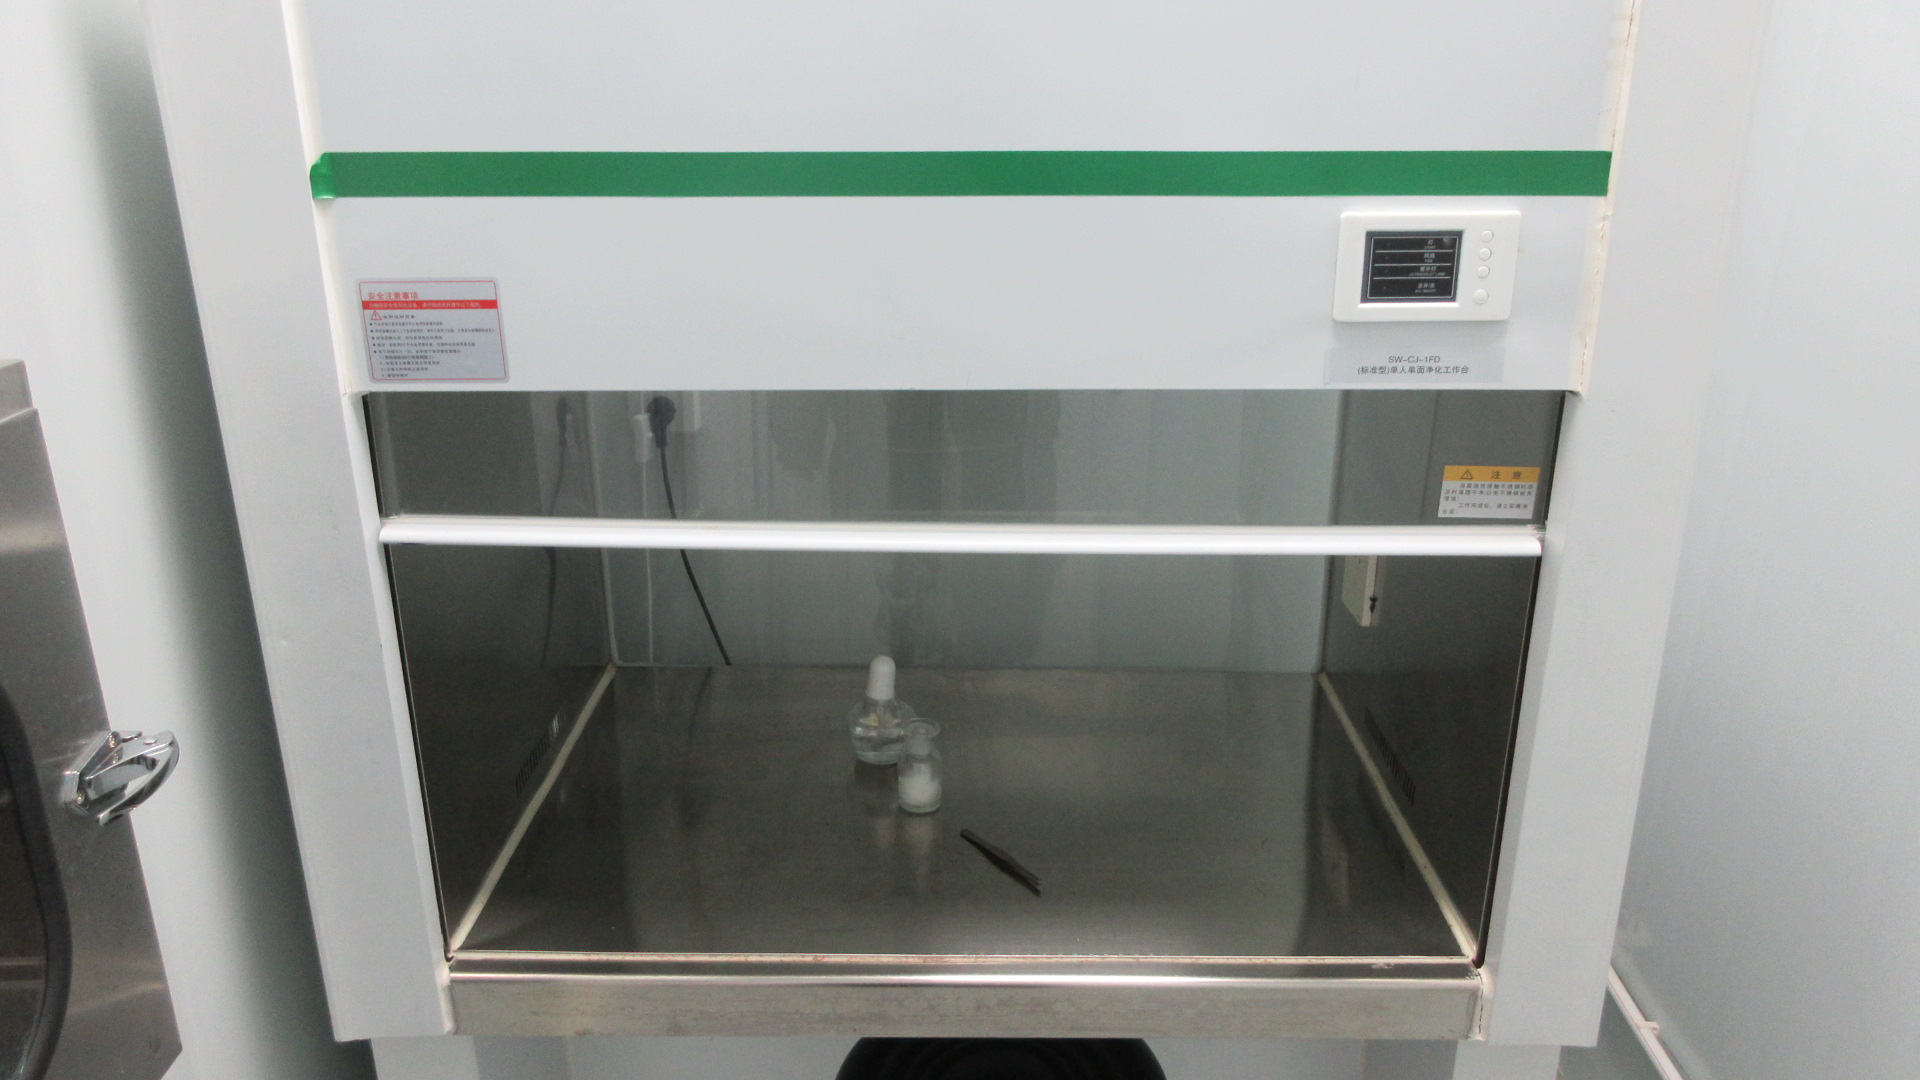
Laminar Flow Clean Bench
HEPA-filtered Class 100 sterile cabinet preventing sampling contamination.
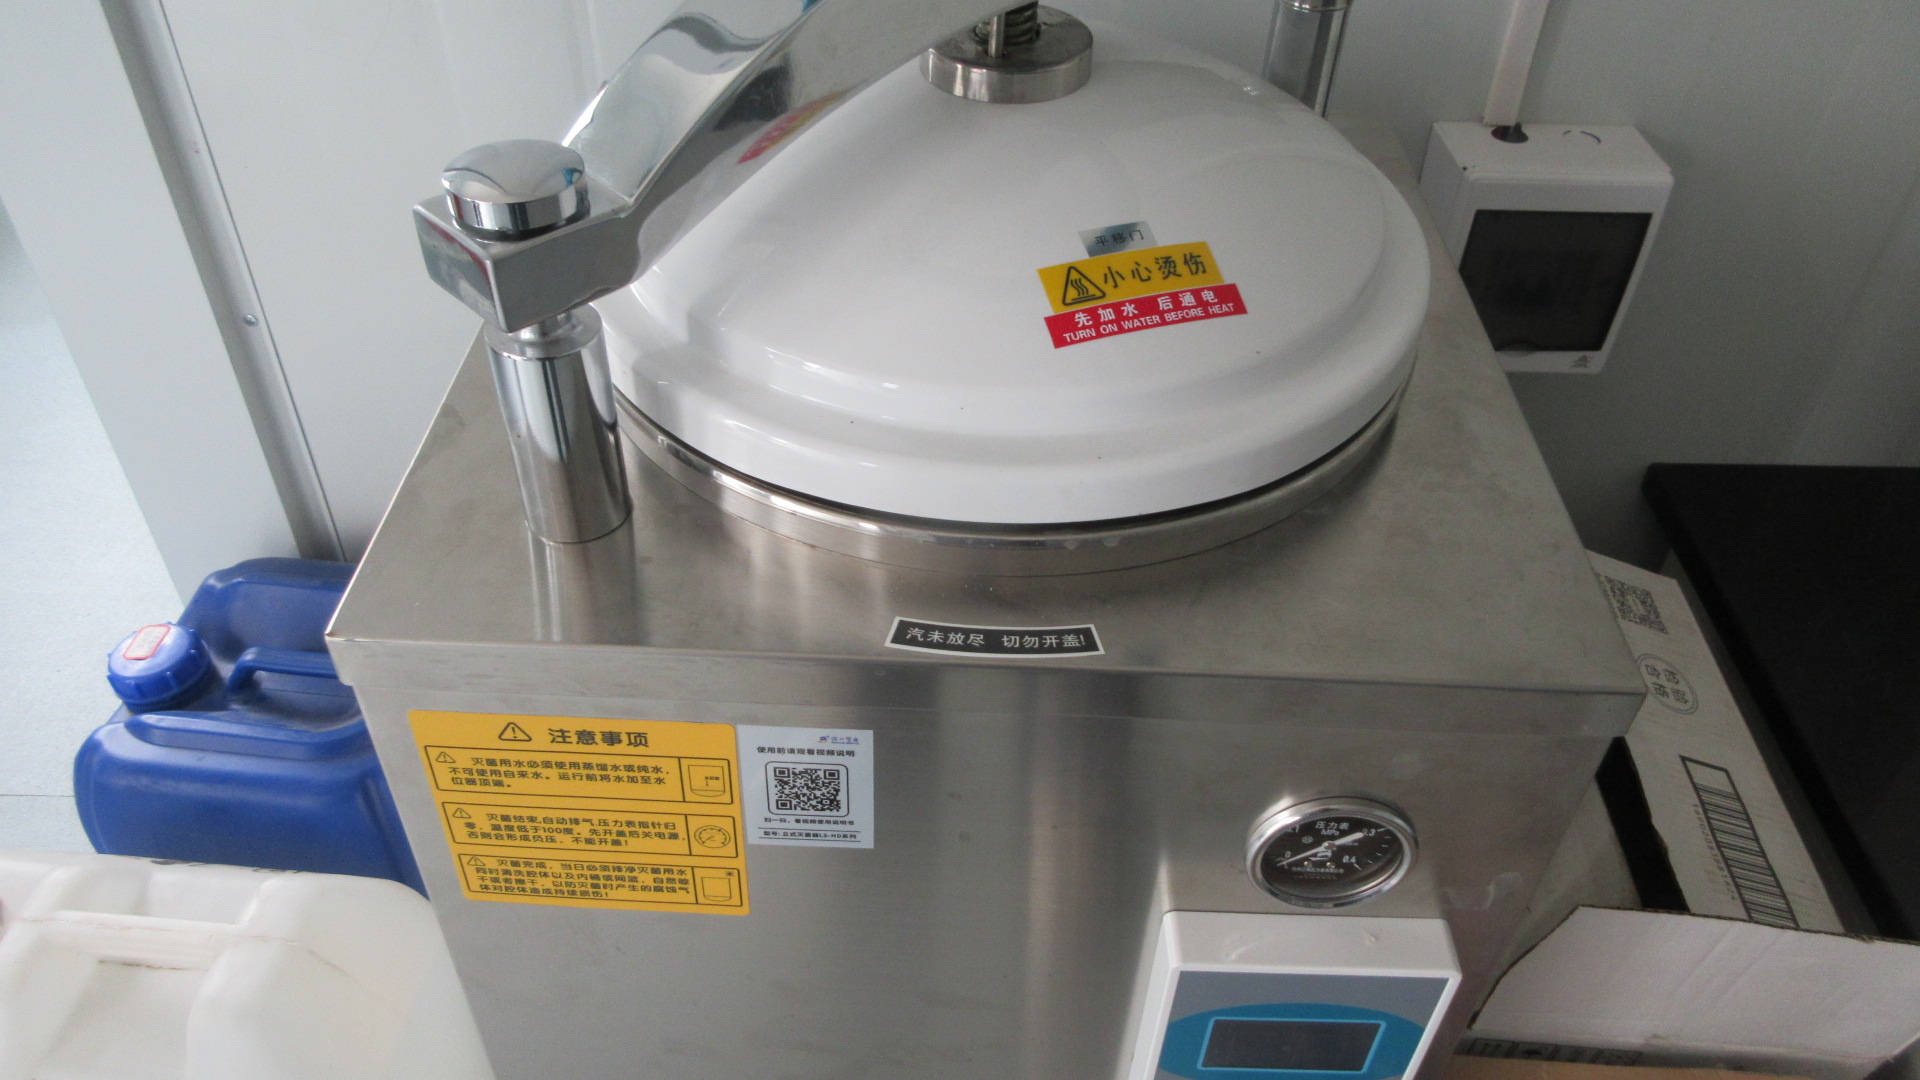
Autoclave Sterilizer
High-pressure steam sterilization for microbiological culture media and equipment.
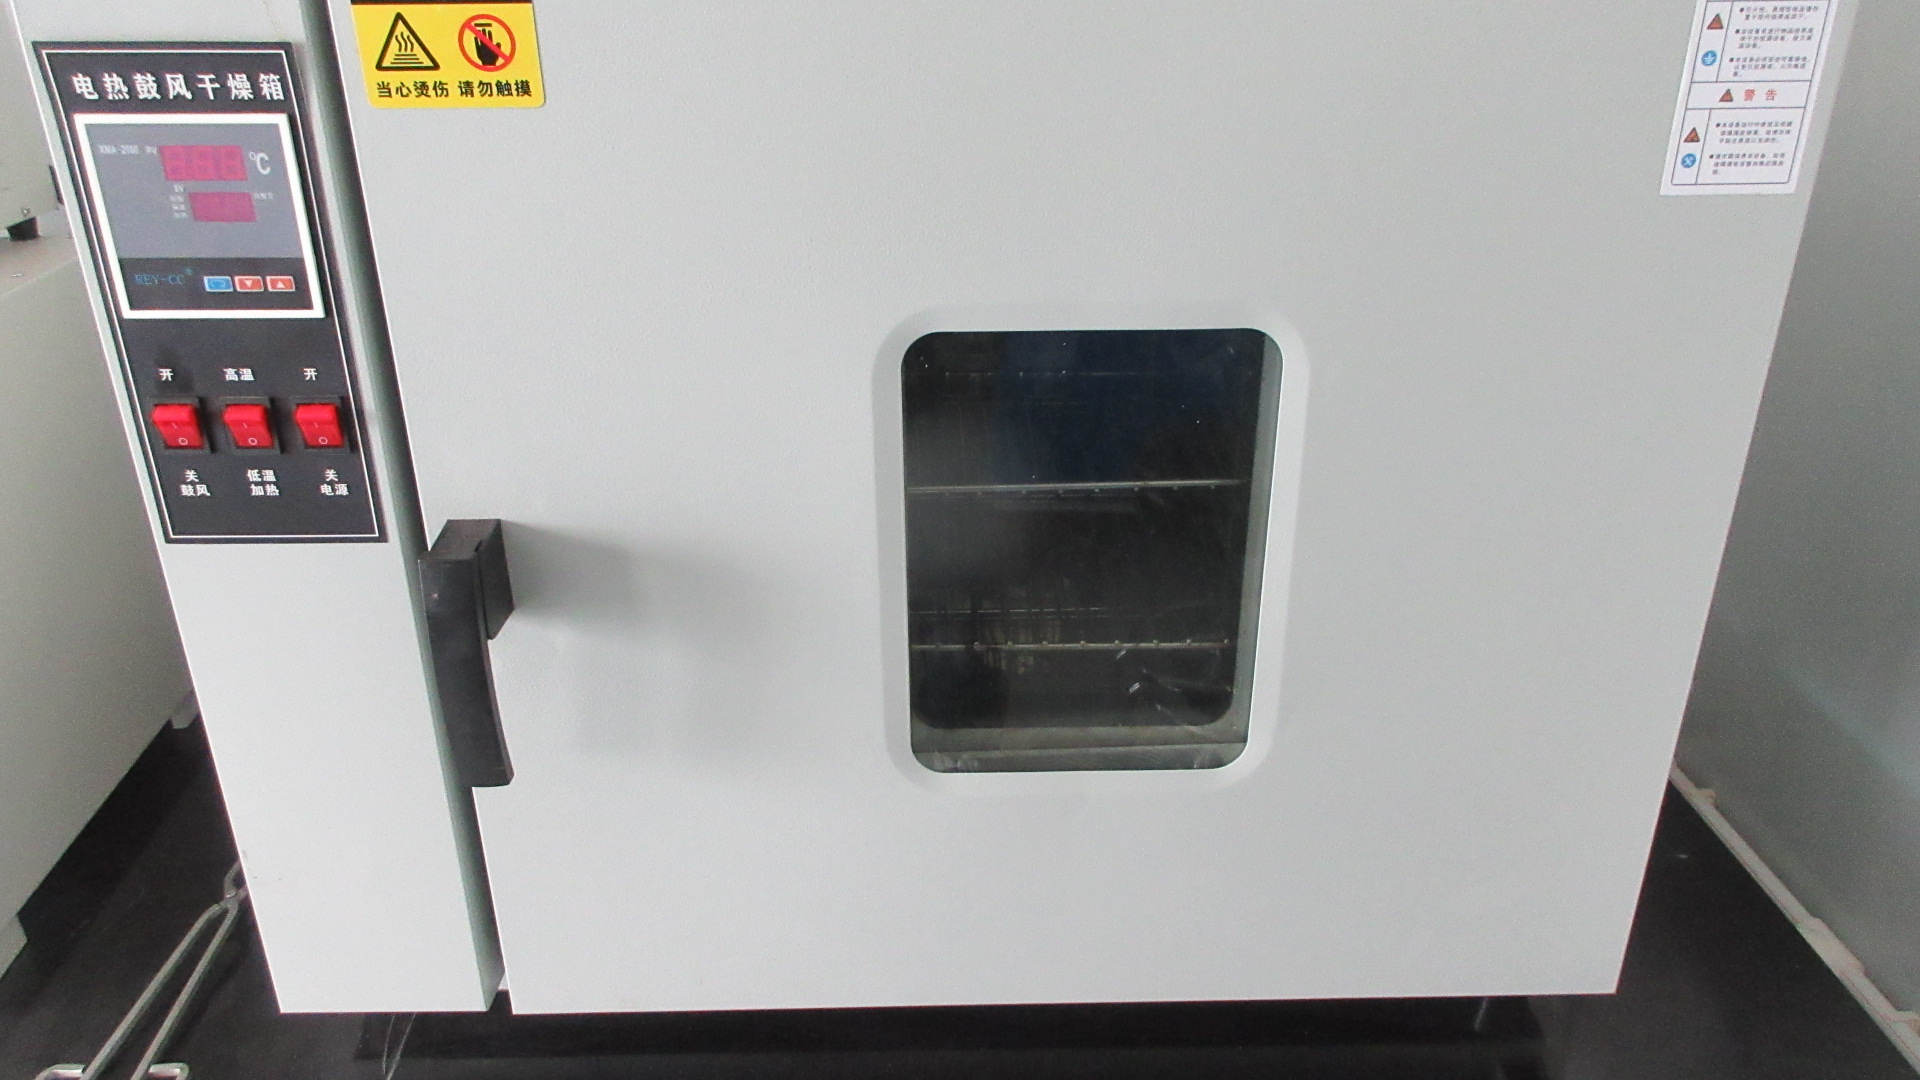
Loss on Drying (LOD) Oven
Exact gravimetric determination of moisture content and ash residues.
Manufacturer Capacities & Global Trade Footprint
Verified capabilities evaluated on-site by third-party auditors and backed by a comprehensive export framework.
Quality Assurance Profile
- QA/QC Inspectors3 Dedicated Staff
- Testing Equipment Types7 Analytical Sets
- Incoming Material RecordsVerified Full Logs
- Supplier Audit SystemOn-Site Audited
- Batch Release ProtocolCOA Every Lot
R&D & Customization
- R&D Formulation Engineers4 Specialists
- Customized on DemandExtract Ratio / Assay
- Sample ProcessingAvailable ≤ 3 Days
- Multi-Compound PremixesCustom Particle Mesh
- Private Label PackagingBottles, Tins, Sachets
Trade & Logistics Reach
- Years in Export Trade15 Years
- Total Operating Staff67 Personnel
- North America Market20% Annual Share
- South America Market20% Annual Share
- Europe, SE Asia & Africa25% Market Share
Verified Certifications & Accreditations
Our quality management and food safety frameworks meet stringently enforced international import standards.
ISO 22000
Food Safety Management System covering botanical ingredients & supplements.
Cert: CN25/00001902 (SGS)HACCP
Hazard Analysis and Critical Control Points in plant extract processing.
Cert: 053HACCP2600079ISO 9001:2015
Standardized quality management across full plant operations and documentation.
Cert: 05326Q00215R301HALAL & KOSHER
Muslim-market and Kosher compliant ingredient processing, verified contamination-free.
Cert: SSPY-201318-32160-R3USDA Organic
National Organic Program compliant botanical extracts & fruit powders.
Cert: 271617250806103110EU Organic
Certified organic processing aids and natural vegetable raw materials.
Cert: CN-BIO-154.156-0001868EOS Organic
Ecocert Organic Standard accreditation for European and international trade.
Cert: 271617/240320230446FAMI-QS Verified
Animal feed additive safety and traceability code for international livestock feed.
Feed Additive Audit PassedInitiate Procurement or Factory Audit Discussion
Need a Certificate of Analysis (COA), pilot test sample, or customized extract ratio specification sheet? Contact our English-speaking technical sales team at BKYULA Biotech Co., Ltd.