 English English
Alongside our premium vanilla extract powders, BKYULA Biotech manufactures an extensive portfolio of HPLC/UV verified botanical extracts, functional feed additives, and nutritional active ingredients with global export compliance.
 UV Protection
 Liposomal Tech
 Natural Foaming
 Immune Support
 Cell Wall Broken
 HPLC 99% Pure
 Zero Calorie
 Fermented Acetic
Natural vanilla stands as the world's most intricate and economically delicate organoleptic compound. Extracted principally from cured seed pods of Vanilla planifolia Andrews (Bourbon type) or Vanilla tahitensis Moore, natural vanilla comprises far more than isolated 4-hydroxy-3-methoxybenzaldehyde (vanillin). It represents a synergistic matrix of over 250 volatile and aromatic phytochemicals, including 4-hydroxybenzaldehyde, vanillic acid, 4-hydroxybenzoic acid, anisic alcohol, and complex glucoside esters. For industrial food manufacturing, craft patisserie, dairy production, and beverage blending in Oceania, switching from unstable synthetic vanillin synthesized from petrochemical guaiacol or wood lignin to authentic, standardized plant-derived vanilla powder provides unprecedented flavor fidelity, regulatory compliance with clean-label mandates, and prolonged thermal stability during high-temperature baking cycles.
BKYULA Biotech Botanical Standardization Rule: Our natural vanilla powder formulations utilize food-grade microencapsulation technologies and vacuum spray drying protocols. This prevents oxidative volatilization of aromatic terpenes, eliminates clumping in high-humidity atoll environments, and preserves total aromatic retention up to 220°C baking heat.
Traditional vanilla processing relies on prolonged room-temperature ethanol extraction, yielding liquid vanilla tinctures that suffer from volatile evaporation when exposed to industrial heat during commercial biscuit baking or commercial milk reconstitution. At BKYULA Biotech, our Xi'an manufacturing facility bridges cutting-edge industrial extraction lines with gentle drying infrastructure. Raw cured vanilla pods undergo cryogenic milling to rupture botanical cells without inducing frictional heat, followed by multi-stage counter-current aqueous ethanol extraction or state-of-the-art Supercritical Carbon Dioxide (SC-CO2) extraction under precise barometric pressure (25–30 MPa) and temperature (40–45°C). This closed-loop process ensures that heat-sensitive aroma fractions remain uncompromised.
The resulting concentrated vanilla oleoresin is subsequently homogenized with a high-solubility polysaccharide matrix (such as non-GMO maltodextrin, gum acacia, or soluble dietary corn fibers) through high-pressure micro-fluidization. The emulsion is then introduced to low-temperature spray-drying towers operating with filtered HEPA airflow. The outcome is a free-flowing, microencapsulated powder featuring uniform particle size (80–100 mesh) that instantly disperses in both cold water and warm emulsion blends without oily separation or precipitation.
Verified vanillin-to-hydroxybenzaldehyde chromatographic ratios adhering to strict USP and ISO 5565 botanical authentication parameters.
The microencapsulated lipid-polysaccharide casing locks in aromatic volatiles, drastically minimizing fragrance loss in tunnel ovens up to 220°C.
Every industrial production batch undergoes strict isotopic and HPLC testing to confirm absolute absence of ethyl vanillin and banned coumarin additives.
| Analytical Parameter | Natural Vanilla Powder (Food Grade) | Synthetic Vanillin (Petrochemical) | Crude Vanilla Bean Powder (Ground Pods) |
|---|---|---|---|
| Botanical Origin | 100% Vanilla planifolia / tahitensis | Synthetic Guaiacol / Petrochemical | Dried & Pulverized Pod Fibers |
| Primary Active Assays | Standardized Vanillin (1.0% - 5.0% HPLC) | 99.0% Isolated Synthesized Vanillin | 0.8% - 1.8% Variable Raw Vanillin |
| Phytochemical Complexity | 250+ Volatile Phenols, Esters, Acids | Single Monomer (Harsh Flavor Profile) | Raw Phytochemicals + Heavy Fibers |
| Water Solubility | 100% Cold/Warm Water Soluble | Moderate (Requires Alcohol/Solvent) | Insoluble (Leaves Sediment & Specks) |
| Thermal Resilience | High (Microencapsulated barrier) | Poor (Evaporates rapidly >140°C) | Moderate (Fibers scorch at high heat) |
| Moisture Absorption (RH >80%) | Low (Anti-hygroscopic spray dried) | High (Cakes into solid bricks) | Extremely High (Mold risk in tropics) |
Fongafale, the main urban islet of Funafuti atoll in Tuvalu, operates as the administrative, culinary, and commercial nexus of the nation. As an isolated Pacific island nation heavily dependent on maritime imports arriving via the Port of Funafuti, the local food distribution ecosystem faces unique infrastructural challenges: prolonged maritime transit times, extreme relative humidity often exceeding 85%, high ambient temperatures, and maritime salinity. For local commercial bakeries (producing traditional loaves, breakfast buns, and holiday pastries), hospitality caterers, ice cream parlors, and school nutrition programs, procuring food ingredients that deteriorate quickly or spoil due to tropical moisture ingress represents a crippling operational risk.
Liquid vanilla extracts imported in glass bottles suffer from heavy volumetric freight penalties, high breakage rates during maritime transshipment through Fiji or Samoa, and alcohol evaporation when stored in ambient tropical warehouses. Conversely, synthetic vanillin crystals rapidly absorb humidity from maritime air, fusing into solid, unusable clumps within weeks of container unloading. BKYULA Biotech addresses the exact reality of Fongafale importers with our specialized, high-barrier packaging engineering and climate-adapted vanilla powder matrices.
Each unit is vacuum packed with nitrogen gas flushing inside high-density aluminum foil pouches, providing zero water vapor transmission rate (WVTR) against Funafuti's equatorial humidity.
We provide full documentation for transshipment routing via Suva (Fiji) or direct air-express to Funafuti International Airport (FUN), providing customs clearance readiness.
B2B order quantities starting at just 1 kg enable Fongafale merchants, hotel suppliers, and small bakeries to test formulations without committing to excessive containerized inventories.
Our natural vanilla powder delivers multifaceted performance tailored to local processing requirements in Tuvalu:
1. Commercial Bakery & Artisanal Breads: Bakery operations across Funafuti supply daily staples to local communities. Adding BKYULA spray-dried natural vanilla powder at 0.1%–0.3% flour weight yields a rich, warm butter-vanilla aroma that withstands commercial baking cycles. The powder integrates smoothly into bulk flour bins without altering dough water absorption ratios.
2. Reconstituted Dairy & Coconut Milk Beverages: Due to limited pastureland on coral atolls, Fongafale relies extensively on powdered milk, condensed milk, and fresh coconut derivatives. Our cold-water-soluble vanilla powder blends effortlessly into reconstituted dairy drinks, ice pops, and coconut puddings, masking oxidized milk notes and imparting an authentic, creamy custard flavor.
3. Hospitality, Cafes & Eco-Resort Food Services: Catering to visiting governmental delegations, NGO staff, and Pacific travelers, Fongafale's hospitality businesses require clean-label, natural ingredients. Our pure vanilla powder provides the visual cue of natural authenticity and rich floral undertones without synthetic aftertastes.
4. Localized Feed Nutrition & Palatability Enhancement: In artisanal poultry and swine husbandry on Fongafale, feed intake often drops under intense tropical heat stress. Incorporating micro-dosed vanilla aromatic extract powders into premixes stimulates livestock appetite, stabilizing feed conversion rates during heat waves.
Global food safety regulations require transparent traceability. In an era where adulteration of vanilla flavorings with synthetic coal-tar derived vanillin, ethyl vanillin, and dangerous coumarin is prevalent, BKYULA Biotech maintains an uncompromising analytical framework. We operate a dedicated internal analytical testing facility outfitted with multi-channel High-Performance Liquid Chromatography (HPLC), Ultraviolet-Visible (UV-Vis) Spectrophotometers, and Automated Microbiological Incubators.
Every single batch produced for oceanic shipment to Fongafale is subjected to multi-point verification:
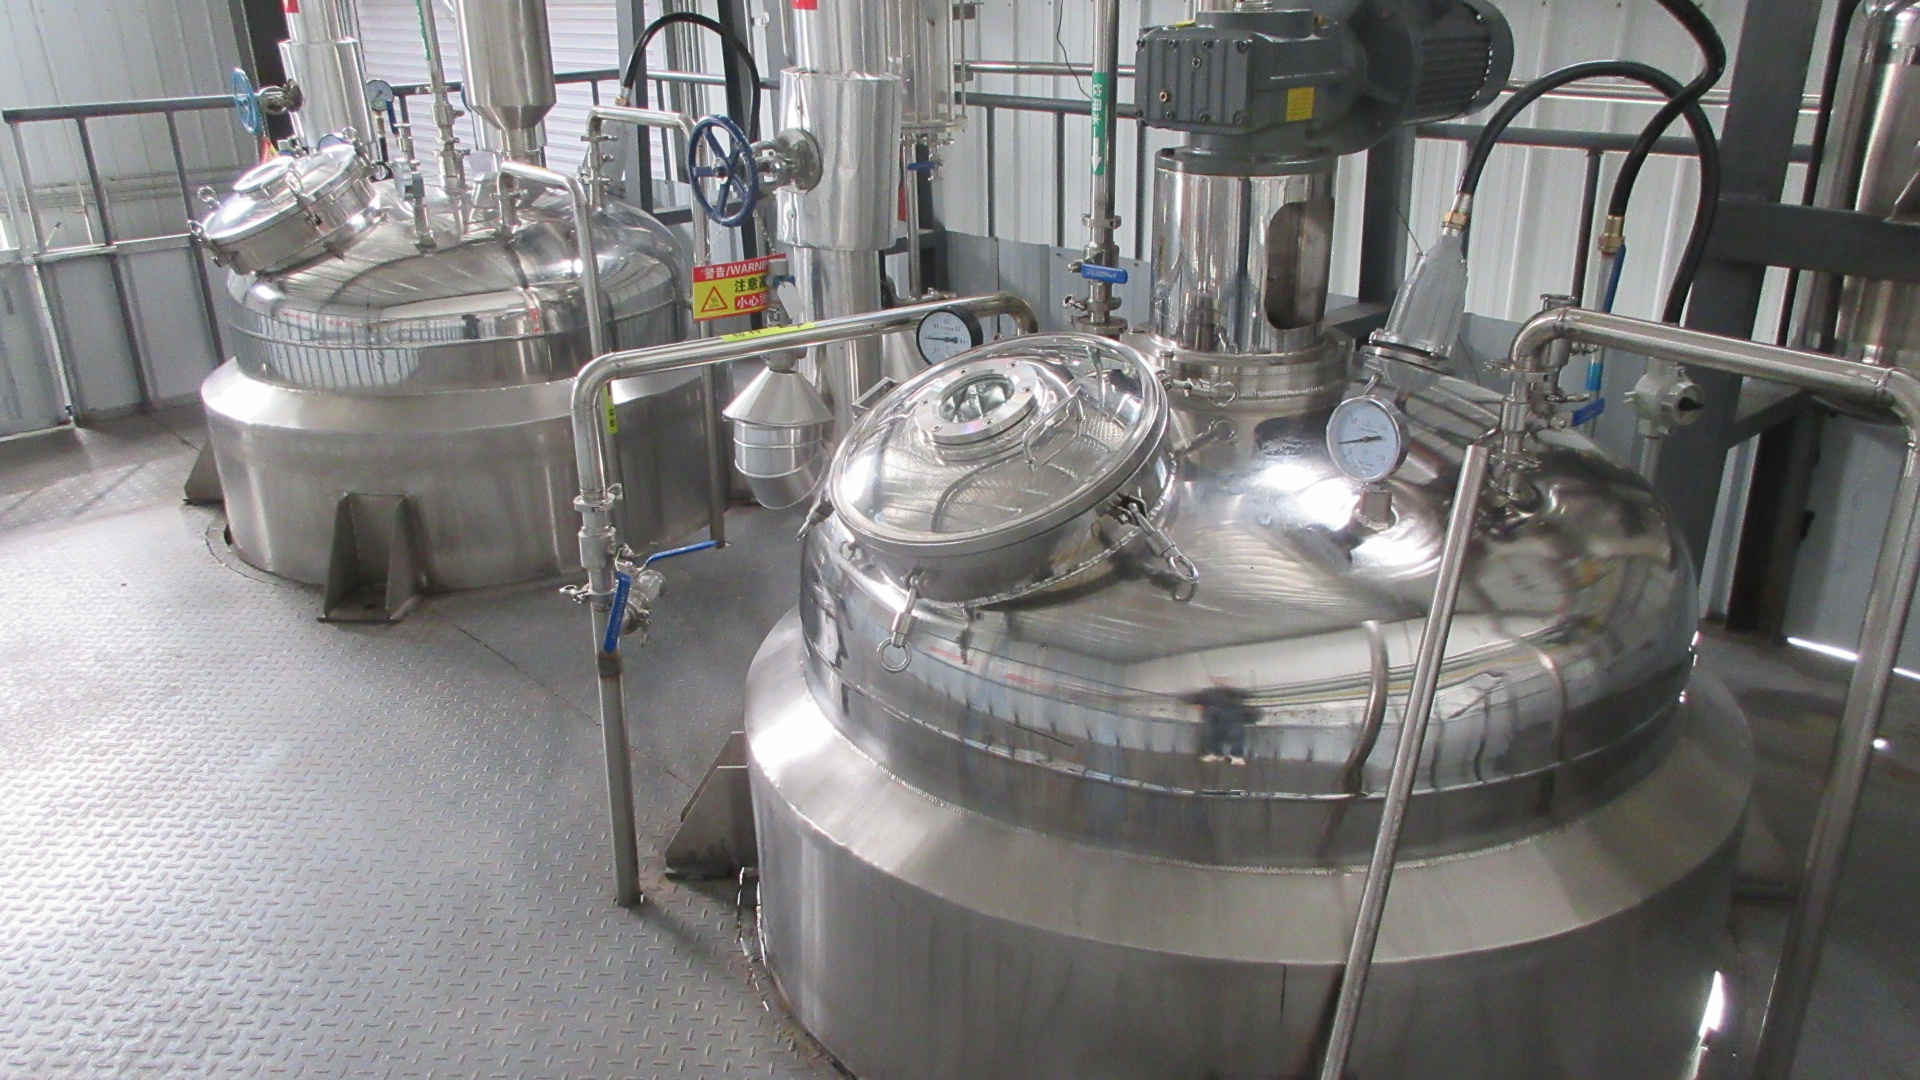
Digital temperature-controlled multi-functional extraction tanks protecting volatile vanilla aroma compounds.
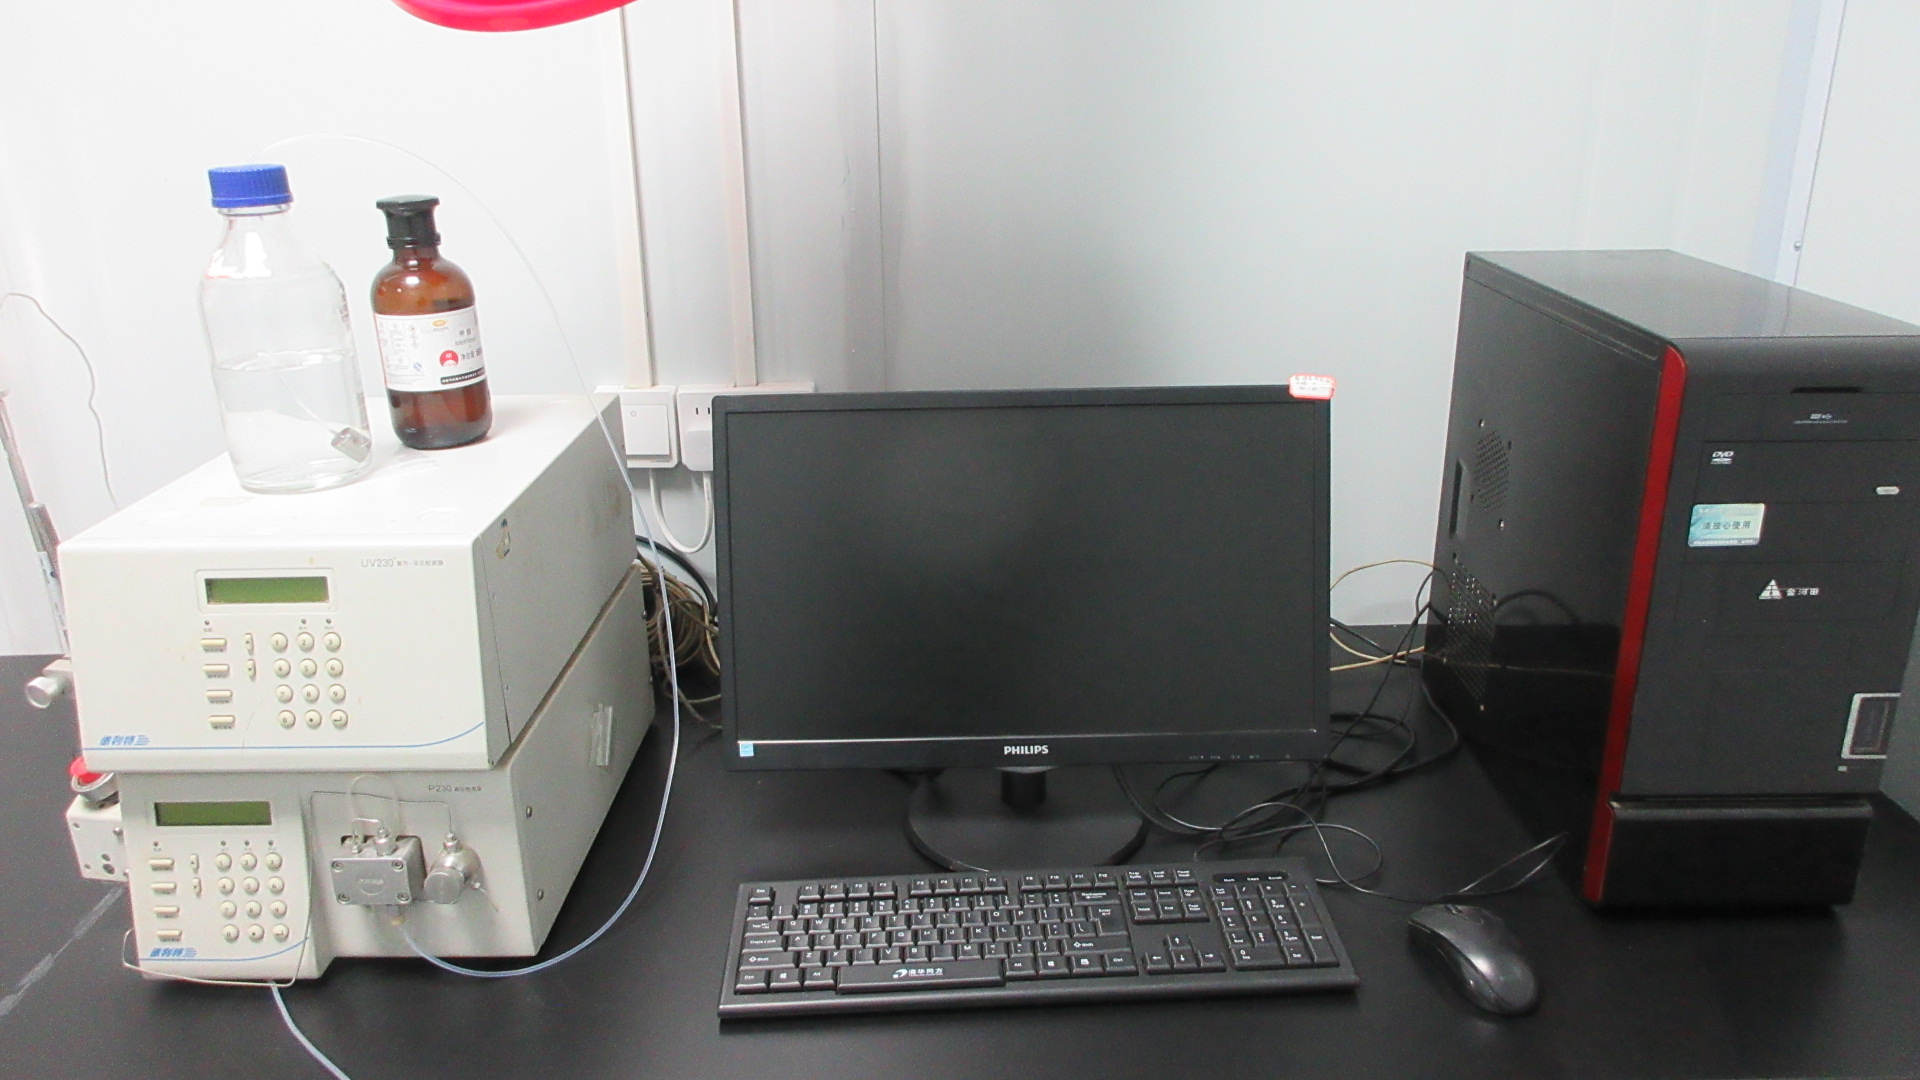
Precise quantification of vanillin percentages and phenolic ratios performed for each shipment batch.
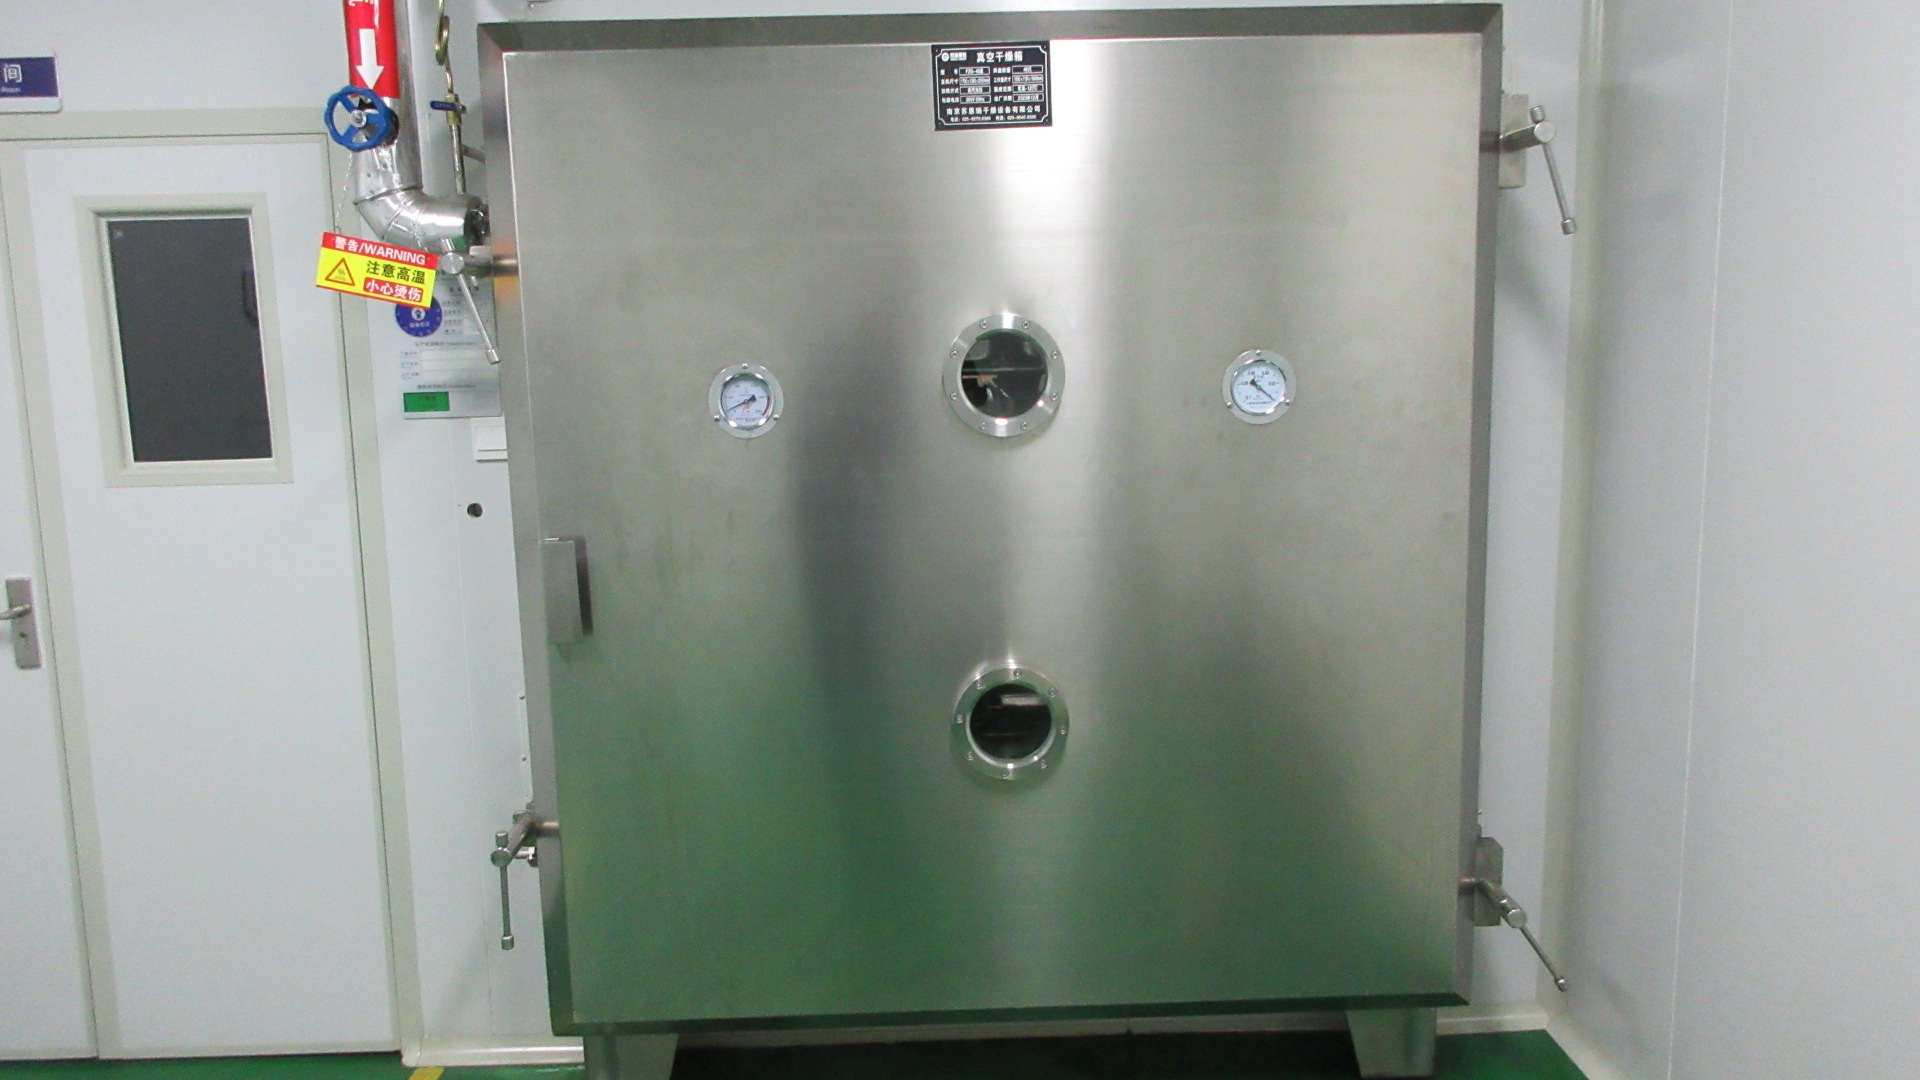
Cleanroom drying infrastructure transforming oleoresin emulsions into free-flowing, anti-caking powders.
Clear, direct answers regarding minimum order quantities, logistics to Tuvalu, documentation, shelf stability, and customized private labeling.
Headquartered in Xi'an, Shaanxi Province, China—the historical cradle of Chinese botanical medicine and modern scientific phyto-extraction—BKYULA Biotech Co., Ltd. has spent over 15 years engineering world-class botanical powders, feed premixes, and specialty food ingredients. Operating across five continents and exporting over US$4.28 million in high-potency extracts annually, we are audited onsite by the SGS Group and adhere strictly to international manufacturing standards.
Operate under ISO 9001:2015, ISO 22000, HACCP, HALAL, KOSHER, and FAMI-QS certified quality management regimes.
Equipped with multi-functional extraction tanks, low-temperature vacuum evaporators, micro-pulverizers, and automated powder blending silos.
Professional technical support team providing comprehensive regulatory documentation, rapid batch sample dispatches, and logistical updates.