English English
Precision-milled, HPLC-tested botanical ingredients, active biological concentrates, and clean-label nutritional powders engineered to comply with strict global food safety criteria.
In modern industrial food formulation, natural vanilla represents not merely an aromatic signature but a pivotal cornerstone of product identity, clean-label positioning, and consumer trust. For manufacturing, dairy, bakery, beverage, and confectionery processors operating in Villa Nueva—the key logistics and industrial epicentre of the Department of Guatemala—procuring bulk vanilla requires balancing intricate flavor chemistry, heat stability, and global regulatory compliance against turbulent global market fluctuations.
This technical whitepaper addresses the procurement architecture required by food scientists, QA directors, and corporate purchasing managers in Villa Nueva seeking sustained partnerships with primary extraction manufacturing facilities in China. By analyzing molecular composition, carrier functionality, spray-drying kinetics, and local manufacturing microclimates, this guide equips industrial buyers with objective technical criteria to optimize formulations, secure supply integrity, and maximize procurement yield.
Under ISO 5565-1 and global pharmacopeial standards, genuine bulk natural vanilla powder is derived directly from cured pods of Vanilla planifolia Andrews or Vanilla tahitensis Moore. Industrial grade powder differs markedly from synthetic ethyl vanillin blends by containing hundreds of secondary aromatic volatile compounds (including 4-hydroxybenzaldehyde, vanillic acid, and p-hydroxybenzoic acid) that create the multifaceted sensory curve consumers identify with authentic premium foods.
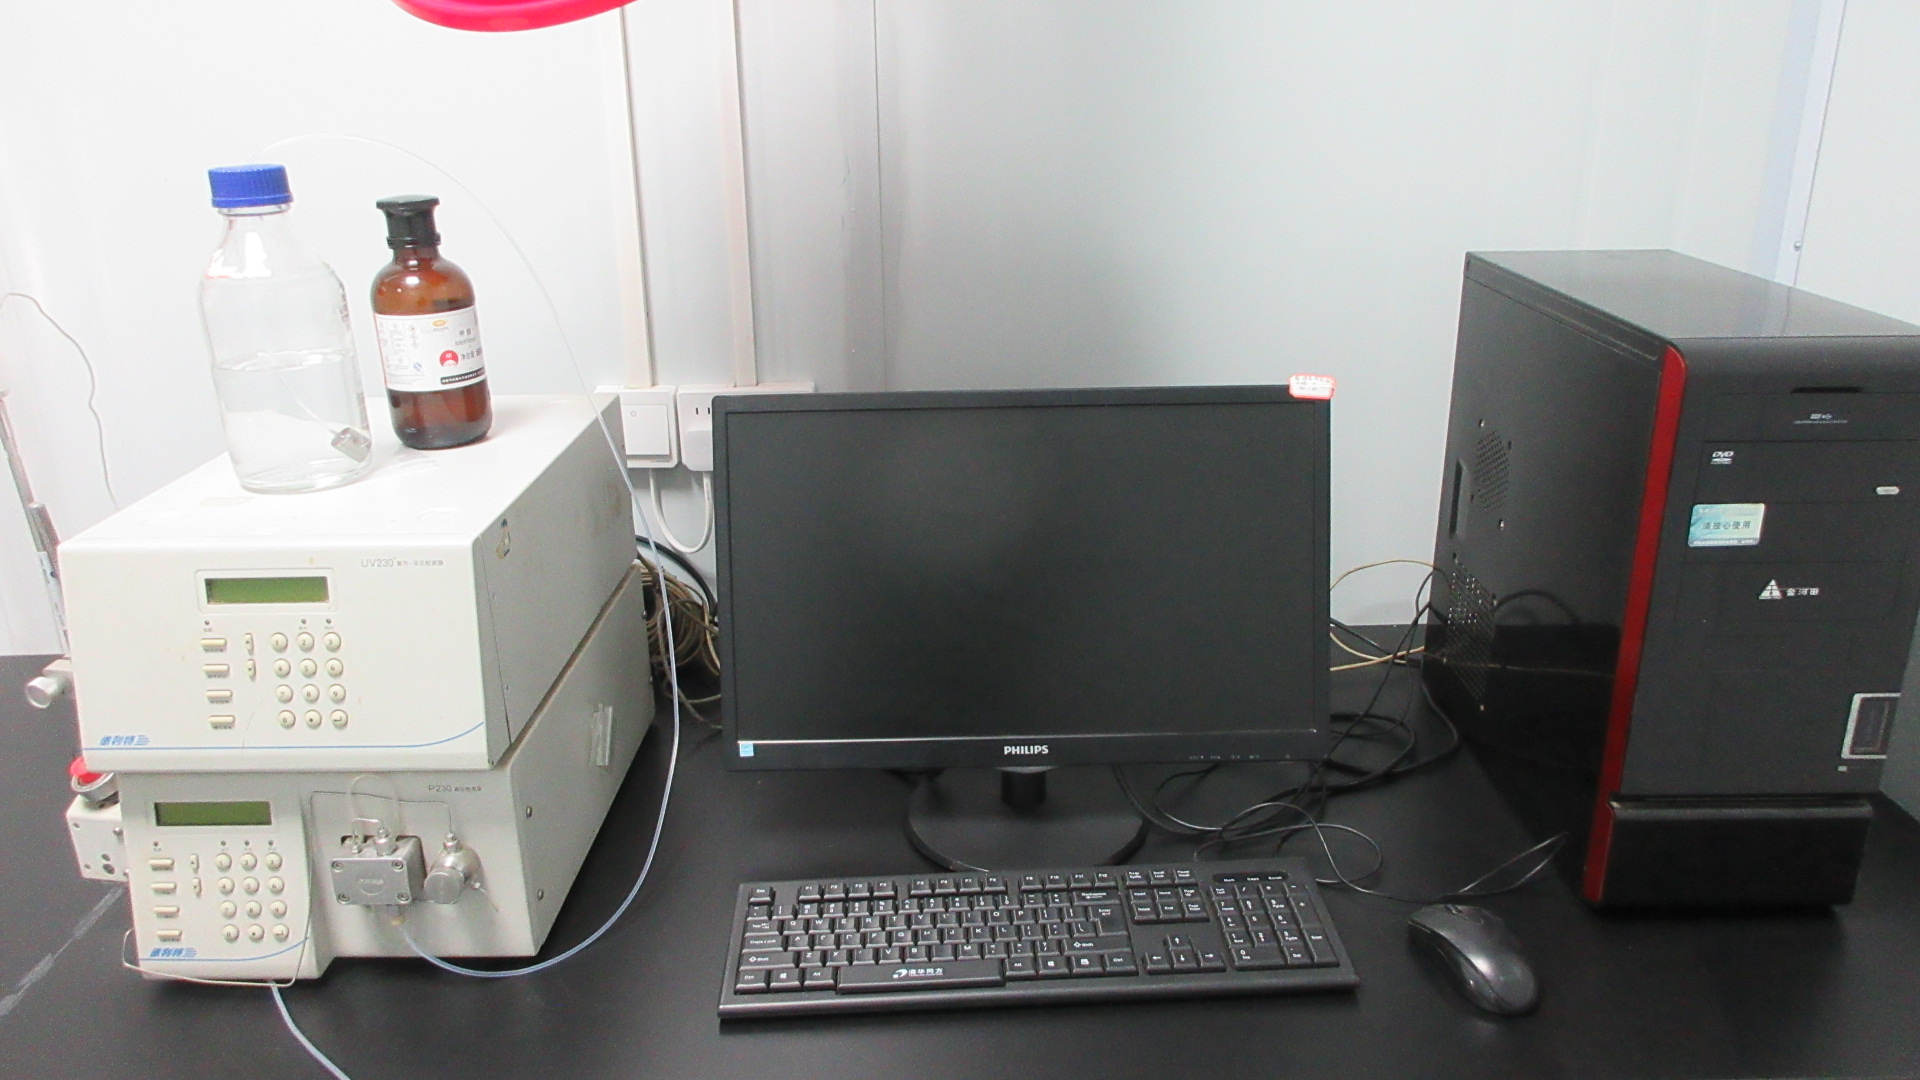
Industrial processors cannot rely on qualitative olfactory assessments; precision manufacturing necessitates rigorous analytical chemistry. The primary marker compound—natural vanillin ($C_8H_8O_3$)—must be quantified via reverse-phase High-Performance Liquid Chromatography (RP-HPLC) linked to diode array detection (DAD) at 280 nm. Beyond the vanillin percentage, the natural botanical authenticity must be certified through carbon isotope ratio analysis ($^{13}C/^{12}C$), confirming that the molecules originate from crassulacean acid metabolism (CAM) botanical sources rather than petrochemical-derived guaiacol or wood-derived lignin.
| Analytical Parameter | Standard Commercial Grade | Premium Botanical Grade | Testing Methodology |
|---|---|---|---|
| Vanillin Content (w/w) | 1.0% - 2.0% Standardized | 2.5% - 5.0% Concentrated | RP-HPLC (AOAC 990.25) |
| Loss on Drying (Moisture) | ≤ 6.0% | ≤ 4.5% | Vacuum Oven Drying 105°C |
| Particle Granulometry | 80 Mesh (180 μm) > 95% | 100 Mesh (150 μm) > 98% | Vibratory Sieve Analysis |
| Bulk Density | 0.45 - 0.60 g/mL | 0.50 - 0.65 g/mL | USP <616> Method I |
| Carrier Substrate | Maltodextrin DE 10-15 | Organic Acacia Gum / None | Enzymatic Digestion / Gravimetry |
| Aerobic Microbial Plate Count | ≤ 5,000 CFU/g | ≤ 1,000 CFU/g | USP <2021> / ISO 4833-1 |
Villa Nueva houses many of Guatemala's most concentrated food processing facilities, spanning high-speed biscuit plants, dairy pasteurization hubs, beverage dry-mix blending plants, and specialty nutritional processors. The atmospheric environment of Villa Nueva—characterized by subtropical highland climate with elevated relative humidity (frequently exceeding 75% during rainy seasons) and temperatures averaging between 18°C and 28°C—presents unique physical demands on bulk powder handling.
In high-speed commercial bakeries operating in industrial zones like Bárcenas and Parque Industrial El Frutal, powders are exposed to mechanical shear stress and thermal degradation during baking extrusion ($180°\text{C} - 220°\text{C}$). Natural vanilla oleoresin or pure vanilla powders without thermal encapsulation suffer from volatile flash-off, losing upwards of 45% of top-note aromatics through steam distillation during the oven rise phase. Our spray-dried microencapsulated vanilla powder utilizes low-DE non-GMO starch matrices and acacia hydrocolloids that create a protective glass-phase core, effectively shielding delicate aroma volatiles until rehydration and mastication occur in the consumer's mouth.
Similarly, for Villa Nueva's large-scale dairy co-packers formulating long-life UHT flavored milks, ready-to-drink yogurts, and ice creams, water solubility and particle suspension kinetics are critical. Untreated raw vanilla bean specks settle out of suspension, leading to non-uniform appearance and sediment clogging in aseptic packaging lines. Our customized instant water-soluble natural vanilla powder undergoes specialized agglomeration milling, providing rapid dispersion in cold fluid milk phases without sediment formation or viscosity spikes.
Engineered for thermal resilience up to 230°C. Retains core volatile aromatics in crackers, sweet rolls, extruded cereals, and cookies without flavor stripping.
Ultra-fine dispersion eliminates phase separation. Masks base dairy notes while delivering rich, creamy, rounded vanilla undertones in frozen and fluid states.
Perfect for protein powders, meal replacements, and instant beverage sachets. Seamless integration with pea, whey, and botanical actives without caking.
The Latin American and Central American food processing sectors are experiencing a decisive structural pivot toward clean-label reformulations. Consumers in regional markets supplied by Villa Nueva's production lines increasingly scrutinize product declarations, driving purchasing away from artificial vanillin labeled as "artificial flavoring" toward "natural vanilla extract" or "natural botanical vanilla powder." Furthermore, the ongoing regulatory convergence across Central America (under RTCA - Central American Technical Regulations) requires explicit declaration of food additives and origin authenticity.
Simultaneously, the surge in plant-based beverages and sports nutrition across the Northern Triangle has created a technical challenge: masking strong vegetative notes inherent in pea, soy, and hemp protein isolates. Synthetic vanillin tends to impart an aggressive, chemical top note that amplifies bitter taste sensations. In contrast, factory-direct natural vanilla powder contains natural phenolic resins, organic acids, and trace esters that round out mouthfeel and naturally suppress astringency without necessitating specialized masking chemicals.
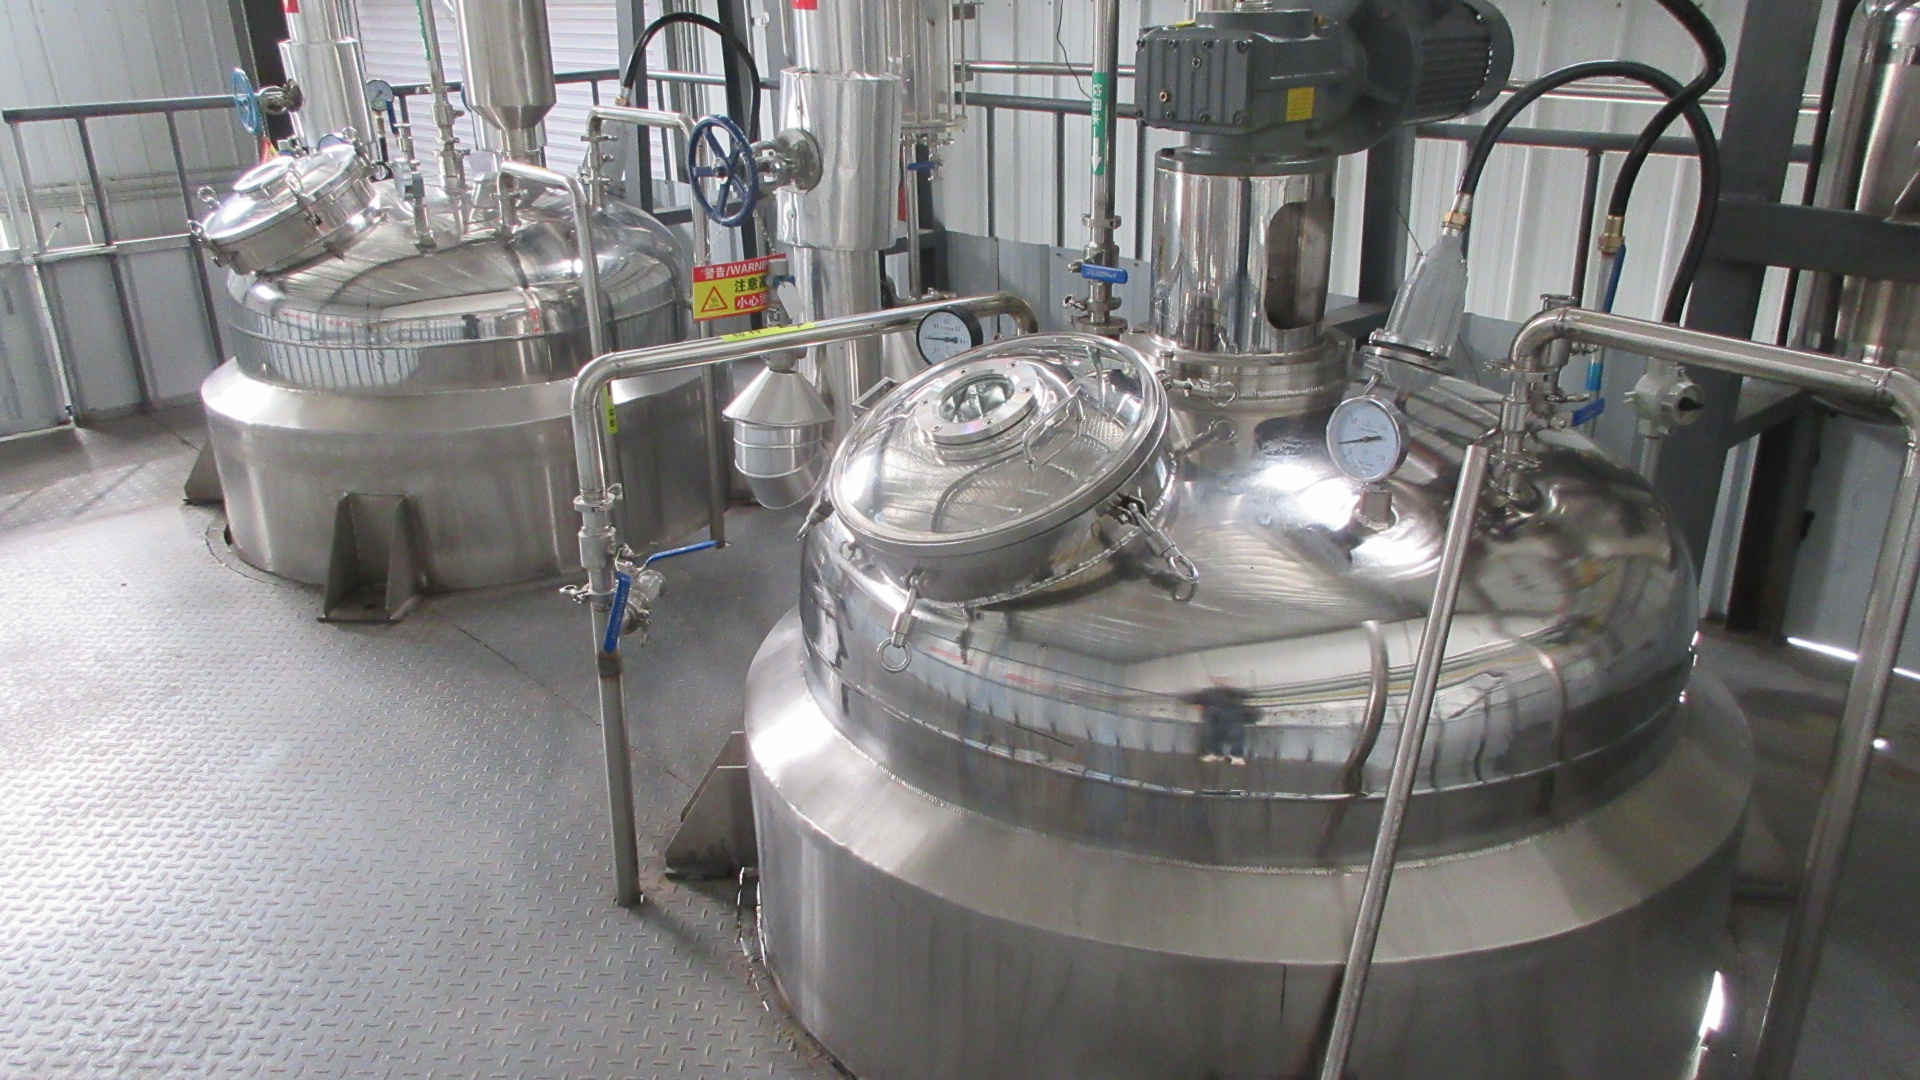
Operating as a primary manufacturer in China's prime botanical extraction hub, our facility leverages multi-stage low-temperature extraction technology to maintain compound integrity. Freshly harvested cured vanilla pods undergo computerized counter-current ethanolic/aqueous extraction inside multi-function stainless extraction tanks. This prevents the thermal breakdown of sensitive phenolic fractions that typically occurs in conventional high-heat decoction methods.
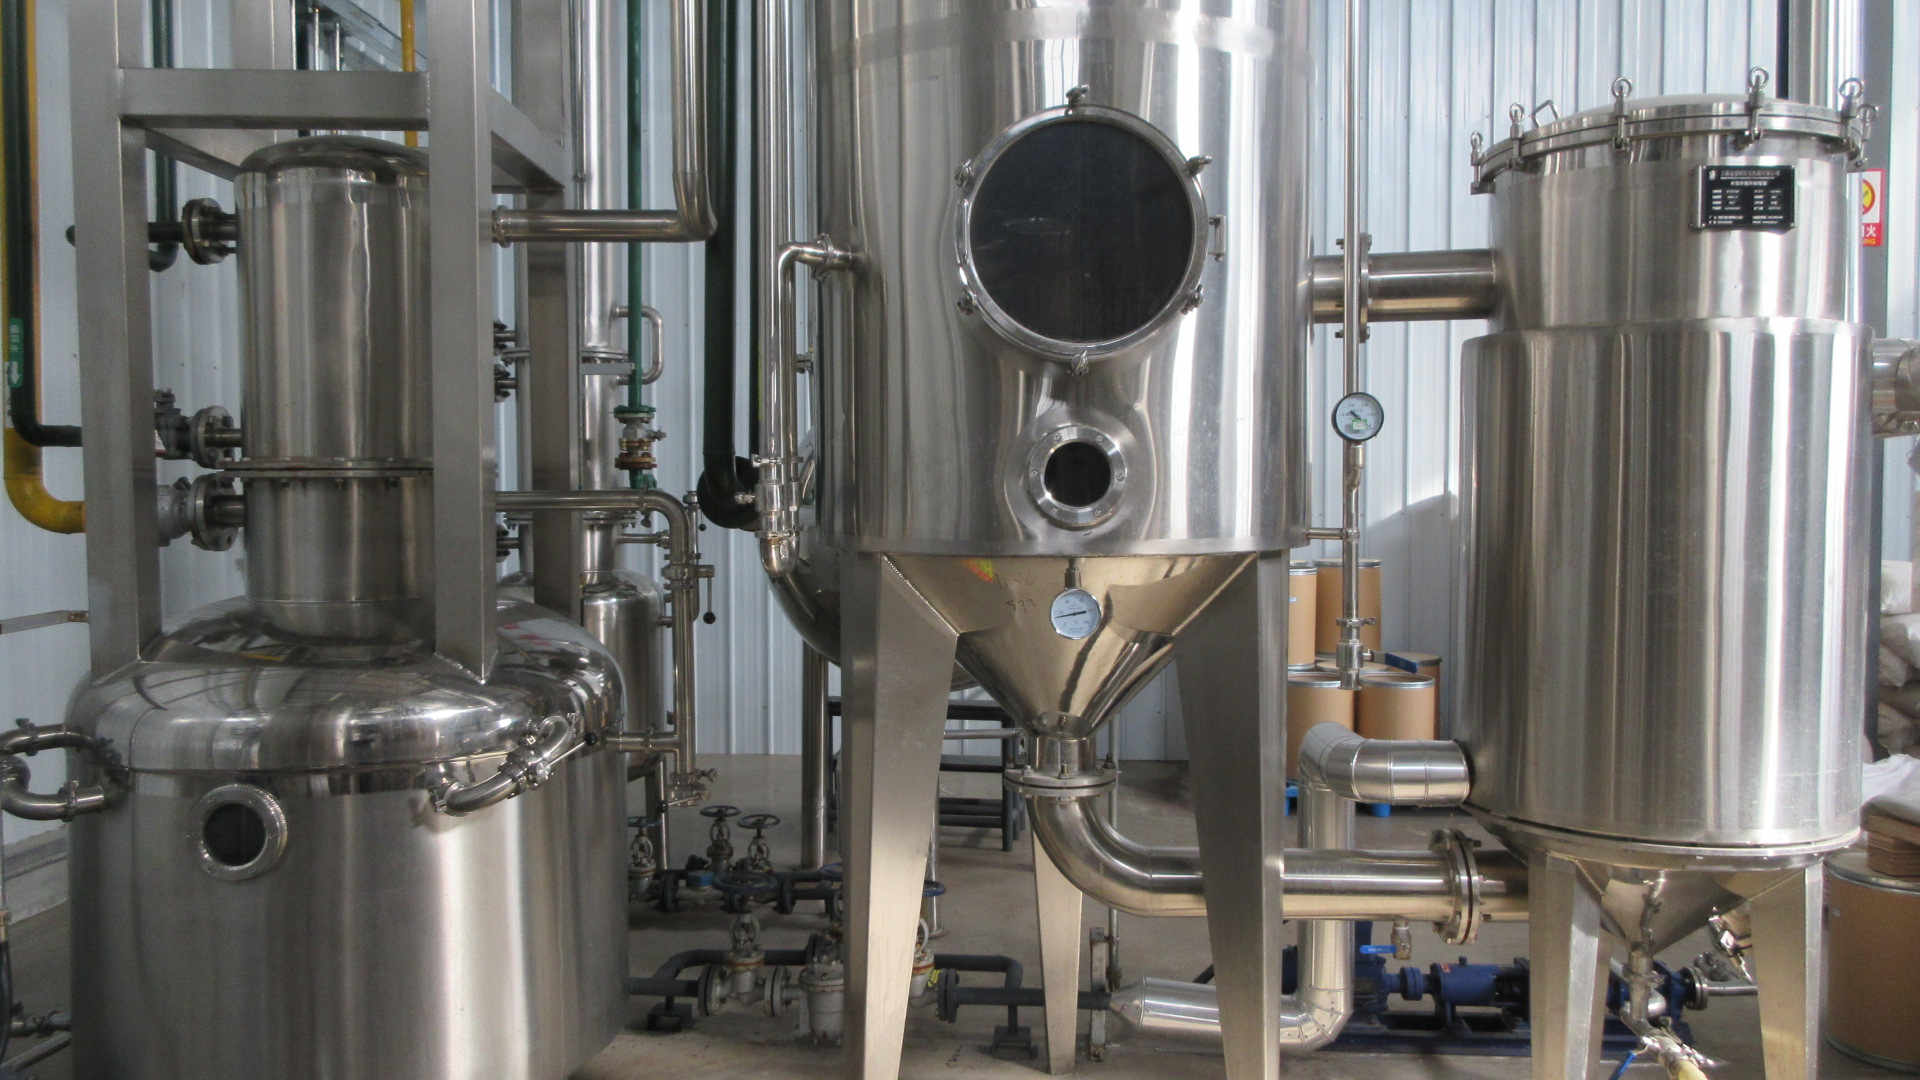
The resulting liquid extract is clarified via disc stack centrifugal separation to remove insoluble cellular debris before entering a falling-film vacuum concentration evaporator operating strictly below 50°C. Once target brix is achieved, the concentrate is micro-fluidized with selected functional carrier agents and spray-dried in sanitary closed-circuit drying chambers. Every step is monitored via integrated SCADA systems, guaranteeing absolute traceability from bulk lot to packaged carton.
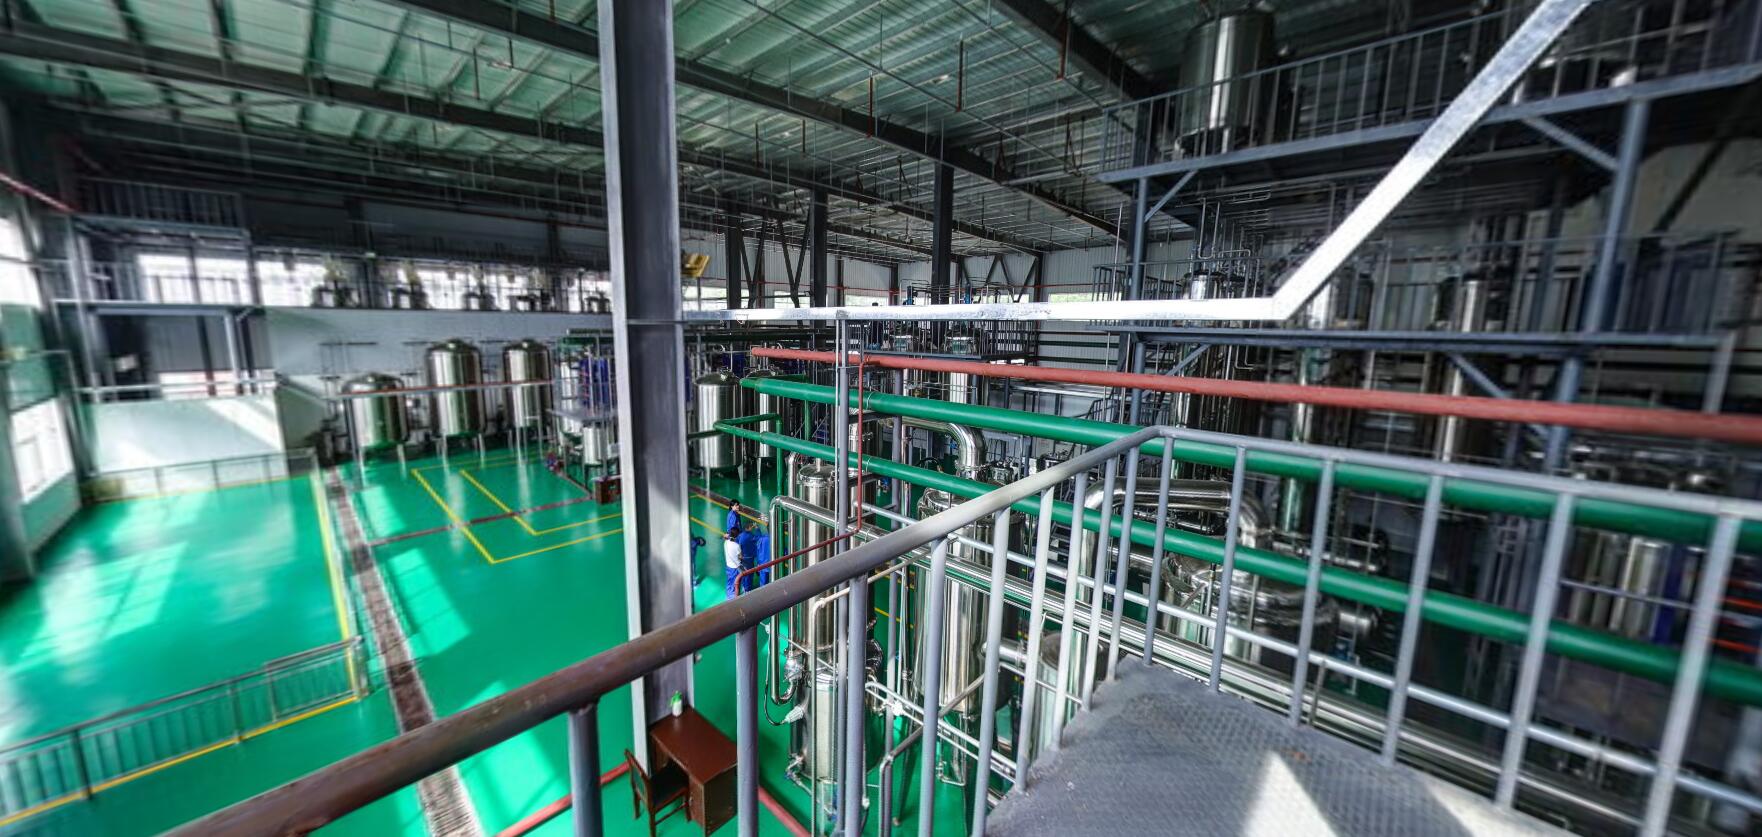
B2B procurement leaders in Villa Nueva require dependable operational predictability rather than middleman brokerage. Sourcing directly from our ISO 9001:2015, ISO 22000, and HACCP certified manufacturing plant delivers distinct commercial and logistical benefits:
Clear, unhedged answers concerning import customs, storage shelf-life, analytical verification, and trial orders for Guatemalan food manufacturing procurement teams.